PCB panelization combines multiple circuit boards into a manufacturing panel, but the breakaway method affects board outline freedom, edge quality and mechanical stress during depanelization. RLX Solutions, a contract electronics manufacturer in Concord, Ontario, reviews panel geometry as part of design for manufacturability (DFM) because V-scoring, tab routing and mouse bites solve different mechanical problems.
V-Scoring Works Best When the Separation Line Can Stay Straight
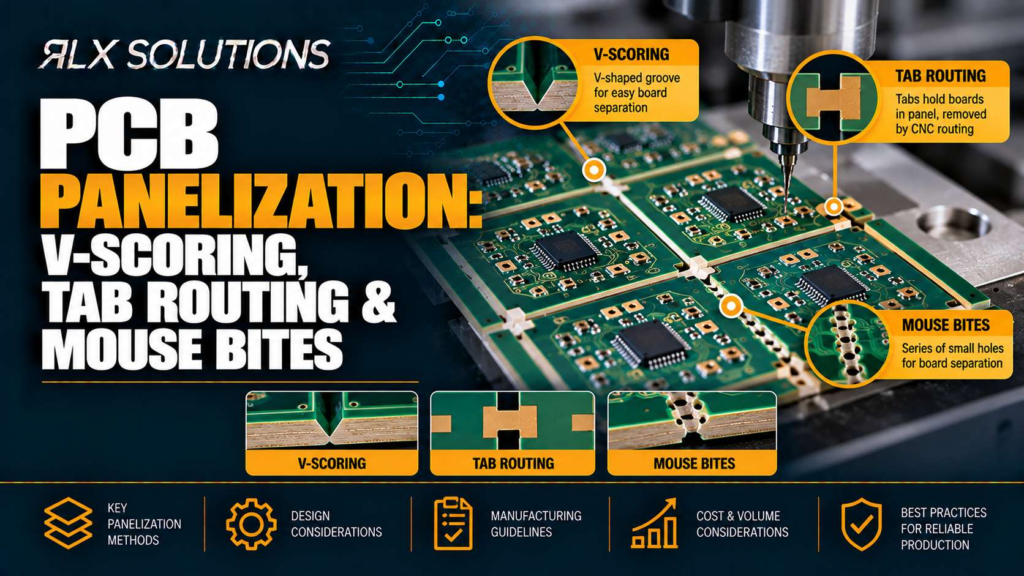
V-scoring creates opposing grooves along a straight separation line, leaving a reduced section of laminate that holds adjacent boards together through fabrication and assembly. After assembly, that remaining web is fractured to separate the boards. For the full picture, see our PCB Manufacturing Guide.
The important constraint is geometric. A scoring blade follows a straight path. It cannot turn around a connector projection, follow an internal radius or selectively avoid one portion of a board edge.
That makes V-scoring attractive for rectangular boards arranged in regular rows and columns. If four 80 × 50 mm boards share continuous straight edges, scoring can establish repeated break lines without routing a complete perimeter around every PCB.
The same simplicity can become a layout constraint. Components, copper and mechanically sensitive structures near the scored edge need to be considered before the panel is released. Breaking the panel applies bending force through the laminate, and that force does not stop exactly at the score line.
A multilayer circuit board with brittle components near the edge deserves particular attention. Depanelization can strain solder joints and component bodies even when the bare board itself survives without visible damage.
A Simple Rectangular Panel
Consider a hypothetical 1.6 mm thick, 4-layer PCB measuring 60 × 40 mm. Six boards are arranged as two rows of three, with straight shared boundaries.
The geometry suits scoring because every intended separation is linear. There is no need to route around an irregular projection.
Now move a ceramic capacitor so its body sits 1 mm from one break line. The panel geometry has not changed, but the mechanical problem has. Separating that panel bends the board locally, so component placement and the planned depanelization method need to be reviewed together.
This is why panelization is not merely a question of fitting the maximum number of boards into a rectangle. The panel has to survive every process before separation and then separate without damaging the finished assembly.
Tab Routing Frees the PCB Outline From a Straight Cutting Path
Tab routing uses a router to cut around most of the board perimeter while leaving small bridges of laminate connecting the PCB to the surrounding panel or neighbouring boards. Those bridges are removed during depanelization.
Because a router can follow a contour, tab routing handles outlines that V-scoring cannot. Rounded corners, projections, recessed edges and irregular shapes can remain attached to a common manufacturing panel.
The trade-off is that the panel now depends on discrete attachment points instead of continuous material along the separation line. Their location matters.
Too few tabs can allow the board to move or vibrate during handling. Poorly located tabs can place separation force beside a connector, sensitive component or mechanically important edge. The tab also leaves material to remove, so the finished edge may require more consideration than an uninterrupted routed edge.
Routing also consumes space between boards. A panel optimized around scoring cannot automatically be converted to routed outlines without reconsidering board spacing and material utilization.
Board A vs Board B: Same Layer Count, Different Panel Cost Drivers
Consider two hypothetical 8-layer, 1.6 mm boards. Both use 1 oz outer copper and have the same overall 100 × 70 mm dimensions.
| Decision Factor | Board A | Board B |
|---|---|---|
| Layer count | 8 | 8 |
| Thickness | 1.6 mm | 1.6 mm |
| Outline | Rectangle | Irregular outline with side projection |
| Separation geometry | Straight shared edges | Routed perimeter |
| Practical panel method | V-scoring candidate | Tab routing candidate |
| Material between boards | Can use shared straight separation lines | Needs routing space around contour |
| Depanelization concern | Bending along score lines | Force concentrated at remaining tabs |
| Primary manufacturing consequence | Simple repeated linear separation | More routing and deliberate tab placement |
The layer count tells almost nothing about this difference. Board B can require more panel-processing work because its outline forces the fabrication route to travel around the board and preserve selected attachment points.
This is also why comparing PCB quotations only by board area, layer count and quantity can miss an important variable. Panel architecture changes how the bare PCB moves through fabrication and how the assembled board is eventually released.
Mouse Bites Control Where a Routed Tab Breaks
Mouse bites are a row of small holes placed across or near a breakaway tab. The holes reduce the amount of laminate that must fracture when the board is removed from the panel.
They are therefore related to tab routing rather than a completely independent panelization architecture. The router establishes the board outline and leaves the tabs. The perforation pattern establishes a more controlled break region within those tabs.
Hole geometry changes the result. Hole diameter, spacing, tab width and the relationship between the hole row and final board outline determine how much material remains and what the separated edge looks like.
A perforated tab can also leave small laminate projections after separation. That matters when the board edge must slide into a close-fitting enclosure, sit against a mechanical datum or remain cosmetically clean.
Suppose a hypothetical 6-layer board has a 0.8 mm finished thickness and a curved perimeter. A designer places three breakaway tabs around the contour, each perforated by a row of small holes. Moving one tab from an open edge to the area beside a board-edge connector changes the mechanical load path during separation even though the Gerber outline remains otherwise identical.
The useful question is therefore not simply, “Does this panel have mouse bites?” It is where the tabs are, how they fracture and whether the remaining edge condition is acceptable for the finished product.
V-Scoring vs Tab Routing vs Mouse Bites
The three terms describe two primary separation approaches and one way of controlling a routed tab. Learn more about bare PCB fabrication requirements.
| Factor | V-Scoring | Tab Routing | Routed Tabs With Mouse Bites |
|---|---|---|---|
| Separation path | Straight | Can follow complex outlines | Can follow complex outlines |
| Board attachment | Continuous scored web | Discrete solid tabs | Perforated tabs |
| Irregular outlines | Poor fit | Good fit | Good fit |
| Panel spacing pressure | Can be efficient on compatible rectangular layouts | Routing requires space | Routing requires space |
| Break force | Applied along score | Concentrated at tabs | Concentrated at weakened tab sections |
| Edge after separation | Scored break edge | Tab remnants need consideration | Perforation remnants need consideration |
| Main design variable | Score-line geometry | Tab number and position | Tab position plus perforation geometry |
Mouse bites do not make an unsuitable tab location mechanically harmless. They change how the tab fractures. They do not remove the need to decide where the attachment belongs.
Likewise, V-scoring is not automatically preferable because it can produce a dense rectangular array. If the resulting break line runs beside mechanically sensitive components, panel efficiency may be bought at the expense of depanelization risk.
Panelization Starts With the Finished Assembly, Not the Bare Board
The best panel layout works backwards from assembly and separation.
A bare board panel can look perfectly reasonable while creating problems after components are installed. Tall connectors may interfere with depanelization equipment. Components near tabs can see local stress. Board projections may require routed clearance. Tooling rails may also be needed to support handling through assembly processes.
For an assembled printed circuit board, panel geometry can affect solder paste printing, component placement, inspection and subsequent separation. Surface-mount technology (SMT) processes need the panel to remain mechanically stable enough for repeatable handling.
Inspection adds another reason to think beyond the individual PCB. Automated optical inspection (AOI) occurs after reflow on both sides where applicable. The panel needs to remain usable through the required manufacturing sequence before anybody removes the finished boards.
The consequence is straightforward: do not finalize breakaway geometry in isolation and then ask assembly to accept it. Panelization belongs in the DFM discussion while component placement and mechanical constraints can still move.
Keep Copper and Critical Features Out of the Mechanical Problem
Board-edge clearance is part of panel design because routing and final separation create real mechanical boundaries.
For fabrication within the applicable design envelope, copper-to-edge clearance is 0.3 mm minimum. That requirement should be treated separately from the additional mechanical judgement required around a breakaway feature. A design can satisfy copper clearance and still place a fragile component where depanelization strain is undesirable.
Routing adds another geometric consideration. Plated slots are supported from 0.65 mm and non-plated slots from 1.0 mm, but a panel-routing decision should not be confused with an electrical or mechanical slot specified as part of the finished board.
The manufacturer needs an unambiguous finished board outline. Panel rails, routed channels, tabs and other breakaway features should not obscure which geometry belongs to the final PCB.
This becomes more important with boards containing edge connectors, gold fingers or precisely located mechanical features. Hard gold and gold fingers are available with 30 μ″ or 50 μ″ gold and bevel, so the panel architecture needs to preserve the intended finished edge rather than treat every perimeter segment as an interchangeable breakaway location.
Dense Boards Make Depanelization Stress More Important
As component density rises, there are fewer harmless places to bend or fracture the board.
Consider a hypothetical 10-layer, 1.2 mm PCB with a 0.5 mm pitch ball grid array (BGA) near one long edge and a board-to-board connector near the opposite edge. The board outline is rectangular, so V-scoring appears geometrically possible.
Now compare two layouts. In the first, both sensitive packages sit well inside the board and the long edges remain mechanically quiet. In the second, the BGA is close to one proposed score line and the connector is close to the other.
The bare-board geometry is almost identical, but the depanelization problem is not. Bending the second assembly along either long edge places strain closer to populated structures. Moving to a routed panel with deliberately located tabs may create more freedom to choose where separation forces enter the PCB.
That decision also affects inspection. BGAs and other bottom-terminated components can require X-ray inspection after assembly. Panel geometry should support the complete manufacturing and inspection sequence rather than optimize a single fabrication operation.
Panelization Can Change Material Utilization Without Changing the PCB
Procurement teams sometimes see panelization as a fabrication detail because the individual board drawing has not changed. Manufacturing sees something different: the panel determines how many boards occupy a working area and how much material becomes routing channels, rails and scrap.
Two identical PCBs can therefore produce different manufacturing conditions when panelized differently.
Imagine a hypothetical 12-layer 90 × 60 mm rectangular board. Panel option A uses straight shared boundaries suitable for scoring. Option B surrounds every board with routed clearance and holds each PCB with tabs.
The finished circuit board is unchanged. Option B, however, consumes panel area between boards and adds routing operations. If the product does not need the outline freedom created by routing, that extra geometry may provide no useful engineering benefit.
The reverse can also be true. Forcing an irregular product into a scoring-oriented panel merely to increase board density can transfer the problem downstream into mechanical separation.
Panel utilization is therefore an input to cost, but usable assemblies are the objective.
Give the Manufacturer Enough Information to Build the Panel Around Reality
A useful panelization review needs more than the bare board outline. The manufacturer needs to understand what must remain mechanically accessible and what cannot tolerate a breakaway feature nearby.
- Gerber RS-274X, ODB++ or IPC-2581 data for manufacturing geometry
- NC drill data so drilled and routed features can be interpreted correctly
- Stackup documentation and fabrication notes where applicable
- An assembly drawing showing component orientation and mechanical relationships
- Bill of materials (BOM) and pick-and-place or centroid data for assembled boards
- Explicit mechanical requirements where a finished edge interfaces with an enclosure, connector or other assembly
Complete information allows the panel to be reviewed as part of the product rather than as a separate rectangle added after PCB layout.
It also reduces ambiguity between a feature that belongs on the finished board and one introduced only for manufacturing. That distinction matters with routed contours, slots, rails and breakaway structures.
Choose the Breakaway Method From the Constraint That Cannot Move
Use the board outline as the first filter. If separation boundaries must curve, step around projections or selectively avoid parts of the perimeter, routed tabs are the natural starting point. Mouse bites can then define a controlled fracture region where appropriate.
For a regular rectangular array with uninterrupted straight separation lines, V-scoring deserves consideration because its geometry matches the panel.
Then apply the assembly filter. A method that fits the outline can still be wrong if separation transfers force into a sensitive region.
Finally, apply the finished-edge requirement. A board that must fit tightly against an enclosure wall, mate at an edge or present a controlled cosmetic surface may make tab location and residual material more important than maximum panel density.
That sequence prevents a common design error: optimizing the manufacturing panel first and discovering later that the assembled product is difficult to separate cleanly.
Put Panelization Into the DFM Review Before Release
Panelization decisions are easiest to change before fabrication files are frozen. If you are preparing a circuit board for quotation, RLX reviews DFM as part of every quote. Send the manufacturing files plus the assembly data when applicable so the proposed breakaway geometry can be considered alongside the board outline, component placement and downstream process.
Frequently Asked Questions
Can V-scoring be used on an irregular PCB outline?
V-scoring is fundamentally a straight-line separation process, so irregular perimeter sections generally point toward routing. A panel can sometimes combine manufacturing techniques, but the proposed geometry should be reviewed as a complete panel. Do not assume that a mostly rectangular board automatically makes every edge suitable for scoring.
Are mouse bites the same as tab routing?
No. Tab routing removes most of the material around a PCB while leaving attachment tabs. Mouse bites are perforations used to weaken a breakaway region in those tabs. Their hole pattern affects how the tab fractures and what remains on the board edge after separation.
Does PCB thickness affect the panelization decision?
Yes. Thickness changes the mechanical behaviour of the circuit board during handling and separation. It should be considered together with panel geometry, tab placement, component locations and the intended depanelization process. Supported rigid PCB thicknesses range from 0.4 mm to 3.2 mm, with ±10% thickness tolerance.
What files should I send for a PCB panelization review?
For fabrication, manufacturing data can include Gerber RS-274X, ODB++, IPC-2581 and NC drill files. Stackup information and fabrication notes should accompany the design where applicable. For assembly work, also provide the BOM, pick-and-place or centroid file and assembly drawing so panel geometry can be reviewed against component placement.
Should components near a breakaway edge be considered during DFM?
Yes. Depanelization introduces mechanical force, so component position relative to score lines and routed tabs matters even when the bare PCB geometry is manufacturable. The review should consider the populated assembly, intended separation method and any mechanically sensitive structures near the perimeter.