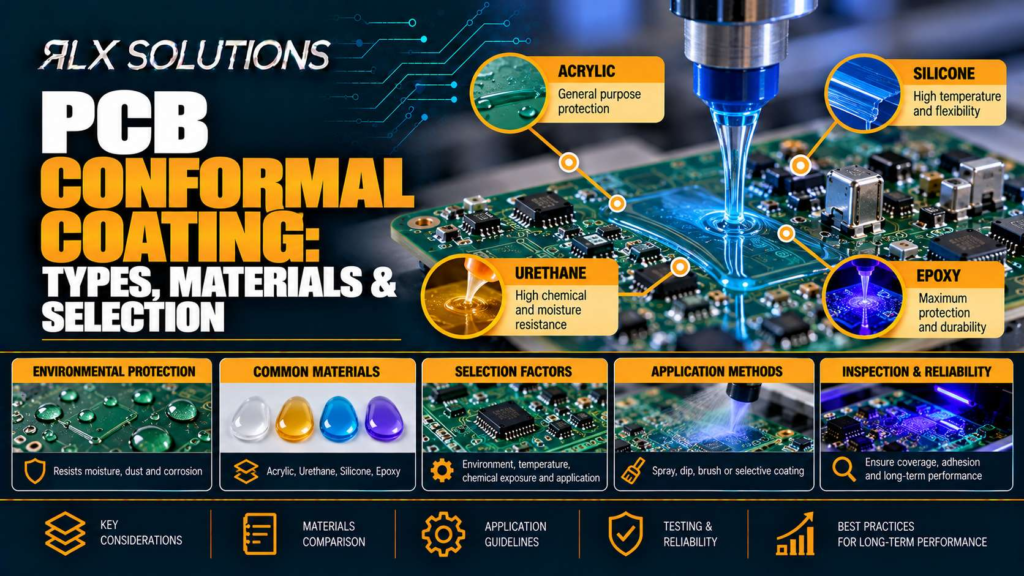
PCB conformal coating is a thin protective material applied over an assembled circuit board to reduce exposure to moisture, contamination and environmental stress. The main material choices are acrylic, silicone, polyurethane and parylene. RLX Solutions, a contract electronics manufacturer in Concord, Ontario, applies coating selection as an assembly decision because material, masking, inspection and rework requirements interact.
Start With the Environment, Not the Coating Name
Conformal coating is intended to follow the contours of components, solder joints and exposed board surfaces rather than form the thick, enclosing mass associated with potting or encapsulation. That distinction affects both protection and serviceability. For the full picture, see our PCB Assembly Guide.
Material selection starts with the actual exposure. A board installed inside a controlled indoor enclosure has a different protection problem from one exposed to condensation, temperature cycling or industrial contamination.
The engineering question is therefore not simply, “Which coating is strongest?” It is whether the selected material and application process protect the vulnerable surfaces without interfering with connectors, test points, heat transfer, mechanical interfaces or later rework.
Consider a hypothetical 6-layer, 1.6 mm circuit board carrying a fine-pitch controller, two board-to-board connectors and several exposed test pads. Full-board coating may cover large areas efficiently, but the connectors and test points still need defined keep-out regions. A selective process can place coating around those exclusions more deliberately. The coating chemistry alone does not solve the masking problem.
That is the first selection rule: choose the protection system, not just the polymer.
Acrylic, Silicone, Polyurethane and Parylene Behave Differently
The four material families solve different combinations of environmental exposure, process control and service requirements. Their practical differences matter after assembly as much as during coating.
| Decision Factor | Acrylic | Silicone | Polyurethane | Parylene |
|---|---|---|---|---|
| General selection driver | Straightforward protective coating where serviceability matters | Temperature and mechanical movement considerations | Chemical and abrasion exposure | Highly uniform coverage of complex geometry |
| Rework consideration | Often comparatively service-friendly | Removal and cleanup require process planning | Rework can be more demanding | Local removal requires a defined process |
| Geometry consideration | Application method controls coverage around components | Material behaviour must be considered around masked areas | Coverage and cure need process control | Deposition can reach difficult geometries |
| Process question | Where must coating be excluded? | How will cure and masking interact with the assembly? | What chemical exposure must the coating resist? | Can every surface that must remain uncoated be protected during deposition? |
These are selection tendencies, not interchangeable performance specifications. A coating should be evaluated against the product’s environmental, electrical, thermal, mechanical and repair requirements rather than selected from the table alone.
Acrylic Coatings Favour Serviceable Assemblies
Acrylic coating is often attractive when a board needs environmental protection while retaining a practical path to repair. That matters for equipment expected to remain serviceable rather than be treated as a sealed module.
The manufacturing consequence appears at masking and rework. Connectors, sockets, contacts and test features that must remain accessible need to be identified before coating. Discovering an undocumented test pad after coating creates an avoidable removal and cleanup operation.
Silicone Coatings Accommodate Demanding Thermal Behaviour
Silicone coatings are commonly considered where temperature variation and mechanical flexibility are significant design inputs. The useful property is not simply “temperature resistance.” The coating and the underlying assembly expand, contract and move, so material behaviour through the expected operating range matters.
This can become relevant around large packages, connectors and mechanically constrained regions. A coating that protects the board environmentally still has to survive the movement generated by the assembly underneath it.
Polyurethane Coatings Suit Tougher Chemical Exposure
Polyurethane becomes relevant when resistance to chemicals and abrasion carries greater weight. That protection can create a corresponding manufacturing trade-off: material that resists its operating environment may also require more deliberate removal when a component underneath needs repair.
Procurement should therefore treat field service strategy as an input to coating selection. A board intended to be repaired repeatedly should not be evaluated solely on initial environmental protection.
Parylene Changes the Application Process
Parylene differs because its deposition process can produce highly uniform coverage over complex board geometry. That can be useful around small features and areas that are difficult to cover consistently using conventional liquid application.
The same coverage behaviour raises the masking stakes. A connector contact, test pad or other functional surface that cannot accept coating must be deliberately protected before deposition. Good coverage becomes a defect if it reaches a surface that was supposed to remain electrically or mechanically accessible.
Application Method Can Decide Whether a Material Works
Conformal coating can be applied across most of the assembly or selectively placed in defined regions. The drawing should make that distinction explicit.
Full-board application can make sense when most populated areas require the same protection and the number of exclusions is limited. Selective coating becomes more attractive as the assembly accumulates connectors, switches, sockets, test pads and other keep-out features.
A coating drawing should identify at least the protected regions and the areas that must remain free of coating. The assembly process then has an executable definition instead of relying on an operator to infer design intent.
The failure mechanism is straightforward. If coating enters a connector interface, covers a required electrical contact or obstructs a test feature, the protective process has changed the functional assembly. Conversely, leaving an unintended gap near a contamination-sensitive region defeats the reason for applying the coating.
Coating Selection Has to Include Masking, Cure and Rework
A conformal coating decision creates a process chain. Each stage can alter the final result:
- Board preparation: Residues and contamination can affect coating behaviour and adhesion.
- Masking: Connectors, contacts, test points and specified keep-outs are protected.
- Application: The chosen process must reach required areas without flooding excluded ones.
- Cure or deposition: The material completes its coating process under controlled conditions.
- Inspection: Coverage, unintended coating and workmanship are checked.
- Rework planning: The repair process must account for removing and restoring coating around replaced components.
This is why a material-only specification is incomplete. “Use polyurethane conformal coating” identifies chemistry but does not necessarily tell manufacturing where it belongs, where it cannot go or what must happen after component rework.
The assembly drawing is the natural place to remove that ambiguity.
Same PCB, Different Coating Strategy, Different Manufacturing Work
Two boards can share the same layer count, dimensions and component population yet require different coating effort because the coating definition changes the post-assembly process.
Take two hypothetical 8-layer boards, each 1.6 mm thick and each using the same 0.5 mm-pitch device.
| Decision Factor | Board A | Board B |
|---|---|---|
| PCB | 8 layers, 1.6 mm | 8 layers, 1.6 mm |
| Fine-pitch device | 0.5 mm pitch | 0.5 mm pitch |
| Coating approach | Broad coating with two connector keep-outs | Selective coating around multiple connectors, test pads and a switch |
| Masking burden | Limited | Higher |
| Application challenge | Broad coverage | Defined boundaries around many exclusions |
| Rework planning | Fewer protected interfaces to manage | More local interfaces affected by coating removal and restoration |
The bare boards may be essentially equivalent from a fabrication perspective. Board B creates more assembly work because coating geometry adds process steps and control points.
This is one reason a PCB quotation and an assembled-board quotation can tell different cost stories. Layer count is visible immediately in fabrication data. Coating exclusions may not become apparent until the assembly drawing and coating requirements are reviewed.
Keep Conformal Coating Separate From Potting and Underfill
Conformal coating, potting and underfill are adjacent processes, but they solve different physical problems.
Conformal coating covers board surfaces and components with a relatively thin protective layer. Potting or encapsulation surrounds a larger portion of the assembly in material, creating a substantially different mechanical and service condition. Underfill occupies the space beneath a package and is used for package-level mechanical support rather than general board coverage.
A design can therefore require more than one of these processes. A component may need underfill while selected regions of the finished printed circuit board receive conformal coating. Treating the terms as substitutes can lead to the wrong drawing notes, material callouts and quotation assumptions.
The repair consequences also differ. Accessing a coated component requires a local coating-removal and restoration process. Encapsulating an assembly can make physical access far more consequential. That distinction should be settled during product design rather than after a failed unit reaches a repair bench.
Component Geometry Changes the Coating Problem
Conformal coating does not land on a flat drawing. It has to move around three-dimensional packages, leads, connectors and board edges.
Tall components can create shadowed regions depending on the application method. Closely spaced features can change material flow. Open connectors create areas where unwanted ingress matters. Package edges and terminations can create local coverage conditions that are difficult to judge from a simple top-view coating note.
Imagine a hypothetical board with a 12 mm-tall connector positioned 3 mm from a coating boundary and a 0.5 mm-pitch package immediately behind it. Moving the connector to 8 mm from that boundary does not change the coating chemistry, but it gives the process a different geometric problem. Placement can therefore influence coating manufacturability before material selection changes at all.
For the layout engineer, coating deserves physical keep-outs just as other manufacturing processes do.
Plan Inspection and Test Around the Coating Sequence
The coating process should fit into the wider assembly inspection and test flow. The key issue is access.
Solder paste inspection (SPI) occurs before reflow, while automated optical inspection (AOI) and other assembly inspection steps evaluate workmanship after component placement and soldering. Packages such as ball grid arrays (BGAs), land grid arrays (LGAs) and quad-flat no-lead (QFN) devices can also require X-ray inspection because critical joints are not fully visible from the surface.
Electrical and functional testing create another constraint. If a fixture, probe or technician needs electrical contact with a test point, coating that location before testing can block access. Test strategy and coating keep-outs therefore need to agree.
For example, suppose a 10-layer assembly has 24 production test points, with eight located inside the region designated for coating. If those eight points remain necessary for fixture contact, manufacturing needs a defined solution, such as preserving those locations as coating exclusions or arranging the sequence so required testing occurs before coating. Leaving that decision unstated transfers a design question to the production floor.
Rework Should Be Designed Into the Coating Specification
Rework is where coating decisions made during design become visible.
Replacing a coated component involves more than removing and soldering a new part. The technician must gain access without creating unnecessary damage around neighbouring features, complete the component repair, inspect the work and restore the protective coating where required.
That sequence makes repair frequency an engineering input. If a connector, socketed component or other part is expected to remain service-accessible, coating boundaries can be designed around that expectation.
For procurement, the implication is equally practical. Comparing coating quotations without matching application boundaries, masking requirements and inspection expectations is not an equal comparison. One supplier may be pricing broad coverage while another is pricing a selective process with numerous exclusions.
Specify the Coating Requirement in Manufacturing Data
A manufacturer should not have to reconstruct the coating intent from a material name buried in a note.
The package should communicate the information that changes the process, including:
- Coating material or approved material requirement
- Areas requiring coating
- Keep-out areas and masked interfaces
- Connectors, contacts and test points that must remain accessible
- Any component-specific treatment
- Inspection or acceptance requirements
- Rework and restoration requirements where they are product-specific
The objective is repeatability. If two operators can read the same drawing and reasonably interpret the coating boundary differently, the documentation needs more definition.
For a new build, coating requirements should also be reviewed with the rest of the assembly data rather than added after the core manufacturing process has already been established.
Choose the Material by the Failure You Need to Prevent
A useful selection framework begins with the expected failure mechanism and then works backward into material and process requirements.
If serviceability carries substantial weight, acrylic deserves consideration. If thermal movement is a major design condition, silicone may be more suitable. If chemical and abrasion exposure dominate, polyurethane can move higher in the evaluation. If highly uniform coverage of complex geometry drives the requirement, parylene may justify its different deposition and masking process.
Then test that material choice against four secondary questions: Can the required areas be coated consistently? Can every keep-out be protected? Can the assembly still be inspected and tested? Can it be repaired using an acceptable process?
That sequence prevents a common specification error: choosing a material for one desirable property while discovering later that its application or removal conflicts with the assembly.
Put Coating Requirements Into the Quote Package Early
If conformal coating is part of a new assembled circuit board, RLX can review it with the assembly documentation as part of the quote process. Providing the BOM, pick-and-place data, assembly drawing and clearly defined coating regions gives engineering enough context to review the coating alongside placement, inspection, test and other post-assembly requirements.
FAQ
What is conformal coating on a PCB?
Conformal coating is a protective material applied over selected surfaces of an assembled printed circuit board. It follows the contours of components, solder joints and board features rather than enclosing the complete assembly in a thick mass. Its specification should also define surfaces that cannot be coated, such as designated contacts, connectors or test interfaces.
Should conformal coating cover the entire circuit board?
Not necessarily. Full-board coverage may suit assemblies with relatively few exclusions, while selective application can be more practical when a PCB contains connectors, test points, switches or other interfaces that must remain uncoated. The drawing should clearly define coverage and keep-out regions so manufacturing does not have to infer them.
Can a conformal-coated PCB be repaired?
A coated board can be designed for rework, but the coating adds steps around the repair. The technician needs access to the component, then the repaired region may require inspection and coating restoration. If particular parts are expected to need field or depot service, their location and coating boundaries should be considered during design.
Is conformal coating the same as potting?
No. Conformal coating forms a relatively thin protective layer over board surfaces and components. Potting or encapsulation surrounds a larger portion of the assembly in material and changes physical access much more significantly. Underfill is different again because it occupies the region beneath a package for package-level mechanical purposes.
What files are needed to quote PCB assembly with conformal coating?
For an assembled-board quote, the manufacturing package can include the BOM in .xlsx or .csv format, pick-and-place or centroid data, and the assembly drawing. When coating is required, that documentation should also communicate the coating and keep-out regions clearly enough for the application, masking and inspection requirements to be understood.