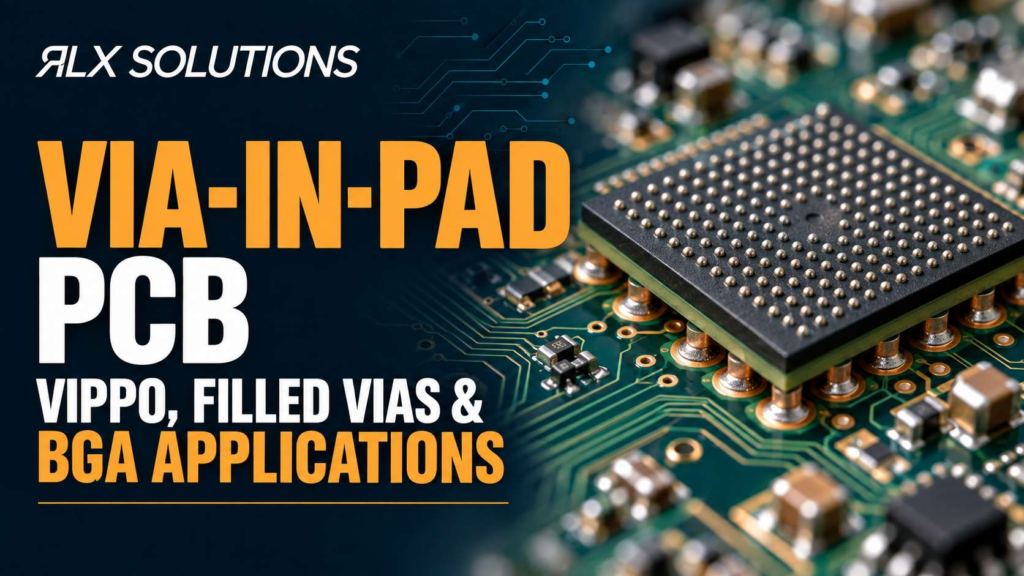
Via-in-pad places a via directly inside a component pad to shorten routing and create escape paths where conventional dog-bone fanout will not fit. For dense BGA layouts, VIPPO adds resin filling, planarization and copper capping so the pad remains solderable. RLX Solutions, a contract electronics manufacturer in Concord, Ontario, reviews this via architecture against the proposed stackup before a board is quoted.
Via-in-Pad and VIPPO Solve Different Manufacturing Problems
A via-in-pad PCB places the drilled via within the copper land used for component attachment. That geometry can recover routing area, reduce interconnect length and move connections vertically without consuming space beside the pad. For the full picture, see our PCB Manufacturing Guide.
But putting a hole inside a solderable pad creates another problem. An open via can pull solder away from the joint during reflow. The hole also interrupts the flat pad surface needed for reliable paste printing and component attachment.
Via-in-pad plated over, commonly called VIPPO, addresses that manufacturing problem by turning the via location back into a substantially planar copper surface. The fabrication sequence includes filling the via, planarizing the surface and applying copper over the filled structure.
That distinction matters in a BGA footprint. “Via-in-pad” describes where the via is located. “Filled via” describes what happens to the hole. “VIPPO” describes a structure in which filling and copper capping support a usable pad surface.
Why an ordinary open via can cause assembly trouble
Consider a 0.5 mm pitch BGA where routing space between adjacent lands is limited. A designer may move a via into the BGA pad to gain an escape route. If that via remains open, solder paste deposited over the land can migrate into the hole during reflow.
The result is not simply less solder. The joint’s solder volume becomes less predictable, while the pad itself is no longer geometrically equivalent to neighbouring pads.
Filling and capping change the mechanism. Instead of asking solder paste to bridge or coexist with a drilled opening, the assembly process sees a copper surface at the via location.
That is why specifying “via-in-pad” alone can be incomplete. The fabrication notes need to communicate the required finished structure.
How a Filled and Capped Via-in-Pad Is Fabricated
VIPPO is a sequence, not one drilling operation. Each added step exists because the preceding step leaves a condition that would otherwise interfere with the finished pad.
- Drill the via. Mechanical drilling may be used for suitable structures, while HDI microvias are laser drilled.
- Plate the hole. Copper creates the required electrical connection through the via structure.
- Fill the via. Resin occupies the remaining opening so the pad does not contain an exposed cavity.
- Planarize the surface. Excess fill material is removed to restore the surface geometry needed for subsequent processing.
- Copper-cap the filled via. Copper covers the planarized via so the component land presents a continuous solderable surface.
- Apply the specified surface finish. The pad then proceeds through the selected finish process with the rest of the circuit board.
Skipping the distinction between these stages can create an ambiguous fabrication package. A note calling for a “filled via” does not necessarily communicate that the final component pad must be copper capped and planarized.
The fill is doing mechanical work as well as closing the hole
Resin fill supports the structure beneath the copper cap. Without an appropriate filled and planarized foundation, the finished pad can retain a depression or surface irregularity.
That geometry matters because solder paste printing depends on the relationship among the stencil aperture, land and component termination. Under a BGA, the joint becomes hidden after placement, so an avoidable pad-surface variable is particularly undesirable.
The copper cap performs a different function. It restores conductive copper over the filled hole and creates the surface onto which the final finish is applied.
For this reason, fill, planarization and cap should be treated as related but distinct fabrication requirements.
BGA Fanout Is Where Via-in-Pad Earns Its Board Area
Via-in-pad becomes valuable when the space consumed by conventional fanout prevents the required number of signals from escaping a BGA.
With dog-bone fanout, a trace leaves the BGA land and runs to a via beside the pad. That via consumes routing space between neighbouring pads and requires enough room for the trace, via land and associated clearances.
Moving the via into the component pad removes much of that lateral geometry. The signal can transition vertically from the pad instead of first travelling sideways to a separate via.
Worked example: 0.5 mm pitch BGA escape
Consider a hypothetical 10-layer printed circuit board with a 0.5 mm pitch BGA. A conventional fanout strategy uses a short trace from each selected BGA pad to a mechanically drilled through via outside the land.
The outer BGA rows may escape cleanly. Deeper rows can become the problem because every additional via consumes part of the routing channel needed by adjacent signals.
A revised version uses filled and capped via-in-pad structures on selected BGA lands. The connection now moves vertically at the pad rather than consuming a separate via position beside it.
If the architecture also requires a 0.10 mm laser-drilled microvia from Layer 1 to Layer 2, the manufacturing sequence changes again. The designer is no longer dealing only with component-pad geometry. The stackup and lamination sequence now participate in the routing strategy.
This is the practical reason via architecture should be decided while the BGA breakout and stackup are being developed, not added as a fabrication note after layout is complete.
Same Layer Count Does Not Mean the Same Via Cost
Layer count is a poor shortcut for comparing two PCB designs when their via architectures differ. Two 10-layer boards can require very different fabrication sequences.
| Decision Factor | Board A | Board B |
|---|---|---|
| Layer count | 10 layers | 10 layers |
| BGA pitch | 0.5 mm | 0.5 mm |
| Main via architecture | Through vias beside pads | Filled and capped via-in-pad |
| BGA breakout | Dog-bone fanout | Vertical transition at selected pads |
| Additional processing | Conventional drilling and plating | Filling, planarization and copper capping |
| Stackup implication | May avoid sequential lamination | Can require additional build stages if blind microvias are introduced |
| Assembly concern | Routing congestion around BGA | Pad planarity and fill/cap execution |
| Primary reason to choose it | Geometry leaves enough fanout space | Routing density makes external fanout restrictive |
Board A should not be converted to VIPPO simply because the technology is available. If conventional vias provide enough escape channels and acceptable electrical geometry, filling and capping every BGA via introduces processing without solving a layout problem.
Board B has the same 10-layer count, but its manufacturing route is different. Each via that becomes part of a component pad has to emerge from fabrication as a suitable solderable land. If the design then adds Layer 1 to Layer 2 microvias or deeper blind structures, lamination strategy becomes another cost and manufacturability variable.
The cost driver is therefore the sequence of processes created by the interconnect architecture, not the layer count printed on the stackup drawing.
Microvias Change the Stackup Before They Change the Layout
Via-in-pad and microvia are not interchangeable terms. A via can sit inside a pad without being a microvia, while a laser-drilled microvia can exist away from a component pad.
The distinction becomes important in high-density interconnect (HDI) designs. Laser-drilled microvias can support stacked or staggered structures, but those structures affect how individual layer groups are formed, drilled, plated and laminated.
Worked example: Layer 1 to Layer 3 connection
Suppose an 8-layer, 1.6 mm hypothetical circuit board needs to move a BGA signal from Layer 1 toward Layer 3.
One layout might use a 0.10 mm Layer 1 to Layer 2 laser microvia and then a staggered Layer 2 to Layer 3 microvia. The second via is laterally displaced rather than positioned directly beneath the first.
Another layout could require a stacked Layer 1 to Layer 2 and Layer 2 to Layer 3 structure. The electrical destination may be similar, but the physical construction is not. The stacked arrangement concentrates the vertical structures at the same XY location and makes fill, cap and registration behaviour part of the manufacturing decision.
A third possibility may use a blind via structure appropriate to the proposed stackup. Blind vias on multilayer builds require sequential lamination, so the board’s build sequence has to accommodate the via before the finished PCB exists.
This is why a drawing that says only “microvia” does not fully define the interconnect. Layer pairs, stacking or staggering, finished geometry and the intended pad construction all matter.
Aspect Ratio Still Matters Outside the BGA Pad
Dense component placement can make the BGA footprint the visual centre of the design, but the rest of the drilling architecture still has to work.
Aspect ratio relates hole depth to hole diameter. As a plated hole becomes deeper relative to its diameter, plating the barrel consistently becomes more demanding.
For example, take a hypothetical 2.0 mm thick board with a 0.20 mm through hole. The depth-to-diameter relationship is 10:1. Change that hole to 0.15 mm without changing the board thickness and the relationship becomes roughly 13.3:1.
Those two holes may occupy nearly the same layout area, yet they create different fabrication conditions.
That calculation is especially useful when an engineer is trying to shrink every via around a dense package. A smaller drill can release routing area while simultaneously making the hole more difficult to plate through the board thickness.
Microvias avoid treating the entire board thickness as one drilled barrel because they connect selected layers. That advantage does not make every deep connection a candidate for a chain of microvias. The layer-transition strategy still has to justify the additional fabrication stages.
Surface Finish and Solder Mask Complete the BGA Pad
A copper-capped via-in-pad still needs the same downstream attention as the rest of the component land pattern. The finished pad surface, solder mask geometry and assembly process work together.
Electroless nickel immersion gold (ENIG) is one available finish for a flat component-pad surface. Other finishes can be appropriate depending on the broader circuit board requirements. The via structure should therefore be considered together with the selected finish rather than treated as an isolated drilling specification.
Solder mask geometry matters for another reason. As BGA pitch decreases, the space available for mask features between neighbouring pads also decreases. A layout can therefore satisfy the copper routing objective and still create a solder mask manufacturing constraint.
The correct design sequence is to evaluate the land pattern, via construction, mask geometry and surface finish as one assembly interface.
That is also why a bare PCB drawing and an assembly package should agree. The fabrication drawing defines what must be manufactured beneath the component. The assembly drawing, centroid data and component information define what will eventually be placed on that surface.
Via-in-Pad Changes Inspection Priorities at Assembly
The most important BGA solder joints are hidden once the package is mounted. Visual inspection cannot directly confirm what happened beneath the package body.
Solder paste inspection (SPI) before reflow can measure paste deposition, including volume, area and offset. After reflow, automated optical inspection (AOI) remains useful for visible features, but a BGA requires another inspection method for the hidden joint field.
Automated X-ray inspection (AXI) can examine BGA connections and support void analysis. That inspection becomes an adjacent consideration when the PCB architecture places filled and capped vias directly beneath solder joints.
The important design lesson is that fabrication and assembly cannot be separated at the BGA boundary. The bare board manufacturer creates the pad and via structure. Stencil printing deposits solder onto that structure. Reflow forms the hidden joint. X-ray then provides visibility into a region that optical inspection cannot see directly.
A design decision made during BGA breakout therefore changes both bare-board processing and the assembly inspection plan.
Specify the Via Structure, Not Just Its Location
A useful fabrication package removes interpretation from the interconnect architecture. The manufacturer needs enough information to determine which holes are conventional plated through-holes, which are blind or buried, which are microvias and which component-pad vias require filling and capping.
- Identify the via types and their intended layer pairs.
- Distinguish through vias from blind, buried and laser-drilled structures.
- State where via-in-pad requires resin fill, planarization and copper capping.
- Provide the proposed stackup and controlled-impedance targets where applicable.
- Keep fabrication notes consistent with the Gerber, ODB++ or IPC-2581 data and NC drill information.
- For assembly, provide the bill of materials, pick-and-place data and assembly drawing alongside the fabrication package.
The reason is contractual as much as geometric. A quote is based on the manufacturing scope represented by the released files. If the drawing implies ordinary vias while the design intent requires filled and capped VIPPO, the missing process is not a minor annotation. It changes how the bare board is built.
Review VIPPO Before the Layout Becomes Expensive to Change
The best time to resolve via-in-pad construction is while BGA breakout, stackup and layer transitions can still move together. Once routing is complete, changing a via from a through structure to a blind or stacked microvia can affect more than one local pad.
If you are preparing a dense BGA circuit board for fabrication or assembly, RLX Solutions includes engineer-reviewed DFM/DFA review on every quote. Submit the manufacturing files, stackup information and, for assembly, the BOM, pick-and-place data and assembly drawing so the via architecture can be reviewed with the rest of the build.
FAQ
Is via-in-pad the same as VIPPO?
No. Via-in-pad describes a via positioned inside a component land. VIPPO refers to a plated-over via-in-pad construction in which the via is filled, planarized and copper capped so the location can function as a solderable pad. The distinction matters because simply locating an open via beneath a pad does not provide the same finished surface.
When should I use via-in-pad under a BGA?
Via-in-pad is useful when conventional fanout consumes too much space, when BGA pitch limits escape routing, or when a short vertical transition provides a useful electrical or layout advantage. If a dog-bone breakout fits comfortably and meets the design requirements, adding fill and cap processing may provide little benefit.
Can a BGA via-in-pad use a microvia?
Yes. A laser-drilled microvia can be located inside a BGA pad when the stackup and interconnect architecture support it. The important distinction is that “microvia” describes the via structure while “via-in-pad” describes its location. Stacked or staggered microvias introduce additional stackup and fabrication considerations that should be resolved during DFM.
Why are via-in-pad holes filled before copper capping?
The fill occupies the via opening and provides a foundation that can be planarized before the copper cap is formed. That prevents the component pad from remaining an open cavity and helps create the flat copper surface needed for solder paste printing and attachment. Filling and copper capping therefore solve related but different parts of the manufacturing problem.
How should I call out VIPPO in PCB fabrication files?
Identify which vias require the filled and capped structure, define their layer connections, and keep the fabrication notes consistent with the drill data and stackup. For microvias, blind vias or buried structures, identify the relevant layer pairs rather than relying on a generic via note. Complete manufacturing data gives DFM review enough context to evaluate the build sequence.
How are BGA solder joints inspected after assembly?
Because the solder joints sit beneath the BGA package, normal optical inspection cannot directly view the entire joint field. SPI can inspect solder paste before reflow, while X-ray inspection can examine hidden BGA connections after assembly and support void analysis. The inspection strategy should therefore be considered alongside the pad and via architecture.