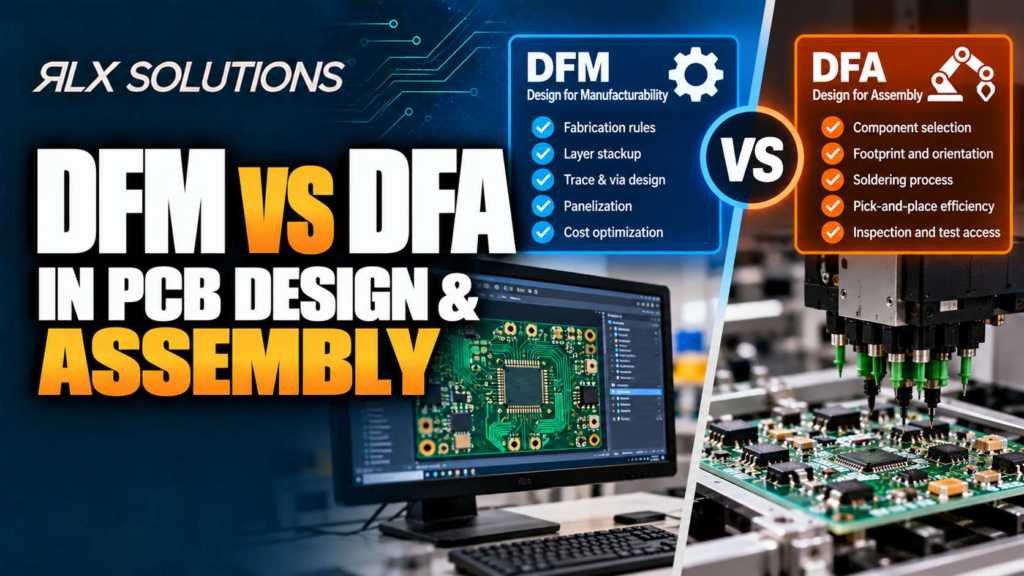
Design for manufacturability (DFM) asks whether your printed circuit board can be fabricated reliably. Design for assembly (DFA) asks whether components can be placed, soldered, inspected and tested reliably. RLX Solutions, a contract electronics manufacturer in Concord, Ontario, applies both because a PCB can pass fabrication review and still create avoidable assembly problems.
The distinction matters most before release. DFM decisions affect the bare PCB: stackup, copper geometry, drilling, vias, solder mask and fabrication tolerances. DFA decisions begin with the populated board: component orientation, land patterns, placement access, soldering, inspection and test.
Treating DFM and DFA as one generic review hides where risk enters the build. For the full picture, see our PCB Engineering Guide.
DFM vs DFA: the practical difference
A board does not become manufacturable simply because every feature can be fabricated. Fabrication and assembly are separate process chains with different constraints.
| Decision factor | DFM | DFA |
|---|---|---|
| Primary question | Can the bare board be fabricated reliably? | Can the board be assembled, inspected and tested reliably? |
| Main inputs | Stackup, Gerbers or design database, drill data, fab notes, impedance requirements | BOM, pick-and-place data, assembly drawing, component geometry |
| Typical concerns | Trace and space, annular rings, vias, aspect ratio, copper-to-edge clearance, impedance, solder mask | Land patterns, orientation, component spacing, paste deposition, solder access, inspection and test access |
| Failure appears | During bare-board fabrication or electrical verification | During placement, soldering, inspection or functional test |
| Cost can increase through | Additional lamination, laser drilling, fill and cap operations, tighter process control | Difficult placement, rework, X-ray requirements, selective processes or poor test access |
| Best time to review | Before fabrication package release | Before assembly package release and preferably while layout can still change |
The useful boundary is simple. If changing a feature changes how the bare board is built, you are primarily dealing with DFM. If changing it affects how parts are placed, soldered, inspected or tested, you are primarily dealing with DFA.
Some decisions affect both.
Via-in-pad is a good example. From a DFM perspective, the via has to be drilled, plated, resin filled, copper capped and planarized. From a DFA perspective, the finished pad must provide a suitable surface for solder paste deposition and component attachment. One layout feature crosses both process chains.
DFM starts with the stackup, not the Gerber viewer
A DFM review should follow the physical manufacturing sequence. Layer structure comes first because it determines what drilling and lamination operations are possible.
Consider a hypothetical 10-layer, 1.6 mm PCB.
Board A uses plated through-holes from Layer 1 to Layer 10. Board B uses Layer 1 to Layer 2 microvias, Layer 2 to Layer 3 microvias and buried vias between Layer 3 and Layer 8.
| Factor | Board A | Board B |
|---|---|---|
| Layer count | 10 | 10 |
| Finished thickness | 1.6 mm | 1.6 mm |
| Via architecture | Through vias | Microvias plus buried vias |
| Lamination dependency | Conventional multilayer sequence | Sequential lamination required |
| Laser drilling | No | Yes |
| Manufacturing stages | Fewer | More |
Both boards have ten layers, so layer count alone is a poor proxy for manufacturing effort.
Board B changes the manufacturing sequence. Blind vias require sequential lamination on multilayer stackups, while microvias introduce laser drilling and may introduce filling and capping operations. The stackup therefore needs to describe the via architecture, not merely list dielectric and copper layers.
This is also why a quote based heavily on board dimensions and layer count can miss an important cost driver. Two files with the same outline, thickness and layer count can require very different process flows.
Hole geometry has to work through the actual thickness
Aspect ratio is the relationship between the depth of a drilled hole and its diameter. As the hole becomes deeper relative to its diameter, plating the barrel becomes more demanding.
Take a hypothetical 2.0 mm thick circuit board with a 0.20 mm through-hole. Ignoring finished-plating details for the simplified calculation, the geometry is approximately 10:1.
Change that same nominal hole to 0.15 mm and the geometric ratio becomes roughly 13.3:1.
Nothing changed in the schematic. The board outline did not change. The layer count did not change. Yet one small drill edit has pushed the fabrication problem into a different process range.
That is DFM reasoning: evaluate a feature in relation to the process that must physically create it.
Good DFM catches interactions between features
Individual design rules are necessary, but many manufacturing problems occur because two individually reasonable choices interact.
Copper weight and trace spacing are one example. A geometry that works with lighter copper cannot automatically be carried into a heavier-copper design because etching has to remove a greater copper thickness while preserving the intended conductor geometry.
Drilling creates another interaction. Hole diameter, board thickness, annular ring and registration have to work together. Shrinking a pad without considering drill position and registration reduces the remaining copper around the hole.
Controlled impedance adds another dependency chain. The trace cannot be reviewed independently of copper thickness, dielectric thickness, dielectric properties and its reference plane. If impedance matters, the manufacturer needs the stackup and impedance target before fabrication decisions are frozen.
The manufacturer therefore needs more than an image of the PCB. A complete fabrication package can include Gerber RS-274X, ODB++, IPC-2581 data, NC drill files, stackup documentation, impedance targets and fabrication notes.
DFA begins where component geometry meets the process
DFA moves the focus from creating copper and holes to depositing solder paste, placing components, forming joints and verifying the result.
A component can fit electrically and geometrically in CAD while creating a difficult assembly condition.
Consider a hypothetical six-layer board carrying a 0.5 mm pitch ball grid array (BGA). The fanout uses conventional vias placed outside the pads. Now compare it with the same six-layer design using a 0.3 mm pitch BGA where routing pressure drives vias directly into selected pads.
The second design creates a chain of consequences.
A via-in-pad structure may need resin fill, a copper cap and planarization so the pad presents a suitable assembly surface. The BGA solder joints are hidden after reflow, so automated optical inspection (AOI) cannot directly inspect the joint beneath the package. X-ray inspection becomes relevant for examining BGA joints and voiding.
The assembly decision has therefore reached backwards into bare-board fabrication and forwards into inspection.
That interaction is why DFA should not be postponed until components have already been ordered and bare boards have arrived.
Assembly inspection should influence layout before release
DFA is partly about making defects less likely. It is also about making the finished assembly verifiable.
Solder paste inspection (SPI) can check paste volume, area and offset before reflow. AOI can examine visible post-reflow conditions. Automated X-ray inspection (AXI) is suited to hidden connections such as BGA and land grid array (LGA) joints and quad flat no-lead (QFN) thermal pads.
Each method sees a different part of the process.
Test strategy adds another constraint. Flying-probe in-circuit test can provide net coverage for prototype and low-volume builds without a dedicated fixture. Bed-of-nails in-circuit testing uses a fixture and becomes a different production decision. Functional test verifies behaviour against the customer-defined test specification.
If test access is considered after routing is complete, the engineer may discover that the electrical test strategy and the physical layout disagree. DFA brings that conversation forward while pads, component locations and routing can still be changed.
DFM and DFA can point in different directions
Optimizing one process in isolation can make another process harder.
Suppose an eight-layer, 1.6 mm board needs dense routing under a fine-pitch BGA. Moving selected vias into pads may release routing space and shorten local escapes. From the layout perspective, the change looks attractive.
From the fabrication perspective, those vias now introduce fill, cap and planarization requirements. From the assembly perspective, the pad surface has to remain suitable for paste deposition and soldering. From inspection, hidden BGA joints may require X-ray verification.
The correct engineering question is therefore not, “Can this feature be fabricated?”
It is, “What process chain does this feature create?”
That distinction prevents local layout improvements from becoming manufacturing penalties somewhere else.
Cost follows process steps more closely than visual complexity
A PCB that looks dense is not necessarily the expensive one. Manufacturing cost follows the operations, controls and verification needed to produce the design.
Return to the two 10-layer boards.
Board A has conventional through vias. Board B adds two microvia levels and buried vias. Their layer counts are identical, but Board B requires a more involved build sequence. If the routing density does not require that architecture, adding it provides no manufacturing advantage.
The same principle applies during assembly. A design that forces difficult solder access, hidden-joint inspection or repeated rework can cost more to build even if its BOM is identical to a more assembly-friendly revision.
This is why DFM and DFA changes are most valuable before procurement and production commitments make a layout change expensive.
Component sourcing belongs in the DFA conversation
The bill of materials (BOM) is not separate from assembly engineering. A footprint, package choice and sourcing decision eventually become a physical part that has to match the land pattern and assembly process.
That matters when an original part becomes obsolete, allocated or otherwise difficult to obtain. A proposed substitute may be electrically compatible while differing in package dimensions, thermal pad geometry or another physical characteristic that affects assembly.
Counterfeit-risk sourcing introduces a different concern. Source vetting, packaging and date-code inspection, visual inspection, lot verification, X-ray and electrical testing can become part of the procurement workflow. If authenticity cannot be established, changing the source is safer than allowing an uncertain component into the build.
A DFA review should therefore connect the BOM, physical package and sourcing plan rather than treating them as independent files.
Class 2 and Class 3 requirements need to enter before production
IPC-A-610 workmanship class affects the acceptance criteria applied to assembled boards, while IPC-6012 addresses printed circuit board fabrication. Class 3 applies tighter requirements than Class 2 in relevant fabrication and assembly criteria.
That distinction should be established before the manufacturer interprets the design and production documentation.
The practical effect reaches into inspection, documentation and process control. First article inspection is particularly valuable because the first completed build creates a checkpoint before the remaining production lot is released.
A design intended for stricter workmanship requirements should therefore carry that intent through fabrication, assembly, inspection and test documentation. Adding the requirement after the build has started does not retroactively change the process used to create the product.
Send DFM and DFA inputs together
The strongest review happens when fabrication and assembly information can be evaluated as one manufacturing package.
For a bare board, that means supplying the manufacturing data, NC drill information, stackup, impedance targets and fabrication notes relevant to the design.
For an assembled PCB, add the BOM, pick-and-place or centroid data and assembly drawing. Native design data can add context when an engineering review needs to trace a manufacturing issue back into the layout.
Keeping these files synchronized matters. A BOM revision paired with an older centroid file can create a different problem from a fabrication error: the manufacturer may be working from individually valid documents that no longer describe the same revision.
Release control is therefore part of manufacturability.
Use DFM and DFA as design feedback, not release paperwork
The highest-value DFM or DFA finding is one you can still act on.
If a via architecture forces extra lamination cycles, discovering that while the BGA escape is still being routed leaves room to consider another fanout. If a package prevents the intended inspection approach, finding it before the BOM and placement data are released leaves room to change the layout or inspection plan.
If you are preparing a printed circuit board for fabrication and assembly, RLX includes engineer-reviewed DFM and DFA review with every quote. Complete manufacturing and assembly files give the review enough context to connect stackup, component placement, inspection and test before production release.
FAQ
Can a PCB pass DFM and still fail DFA?
Yes. DFM can establish that the bare PCB geometry and fabrication approach are manufacturable while the assembled design still creates placement, soldering, inspection or test problems. A via pattern may be manufacturable, for example, while the surrounding component arrangement makes assembly or verification unnecessarily difficult.
Is via-in-pad a DFM or DFA issue?
It is both. Fabrication has to create the via structure, including resin fill, copper cap and planarization where required. Assembly then relies on the resulting pad surface for solder paste deposition and component attachment. For packages such as BGAs, the decision can also affect routing density and X-ray inspection requirements.
What files are needed for PCB DFM and DFA review?
Fabrication review can use Gerber RS-274X, ODB++, IPC-2581 data plus NC drill files, stackup documentation, impedance targets and fabrication notes. Assembly review also needs the BOM, pick-and-place or centroid file and assembly drawing. Native Altium, Eagle, KiCad, OrCAD and DipTrace design data can support engineering review.
Does DFM reduce PCB cost?
It can identify design choices that add manufacturing operations without providing necessary electrical or mechanical value. A through-via design and a microvia design can have the same layer count yet require different drilling and lamination sequences. The useful comparison is therefore the required process flow, not simply the number of layers.
When should DFA be performed?
DFA should happen while component placement, land patterns, routing and test access can still be changed. Waiting until bare boards and components are committed reduces the available fixes. Early review also allows inspection methods such as SPI, AOI and X-ray, plus in-circuit or functional testing, to be considered alongside the layout.