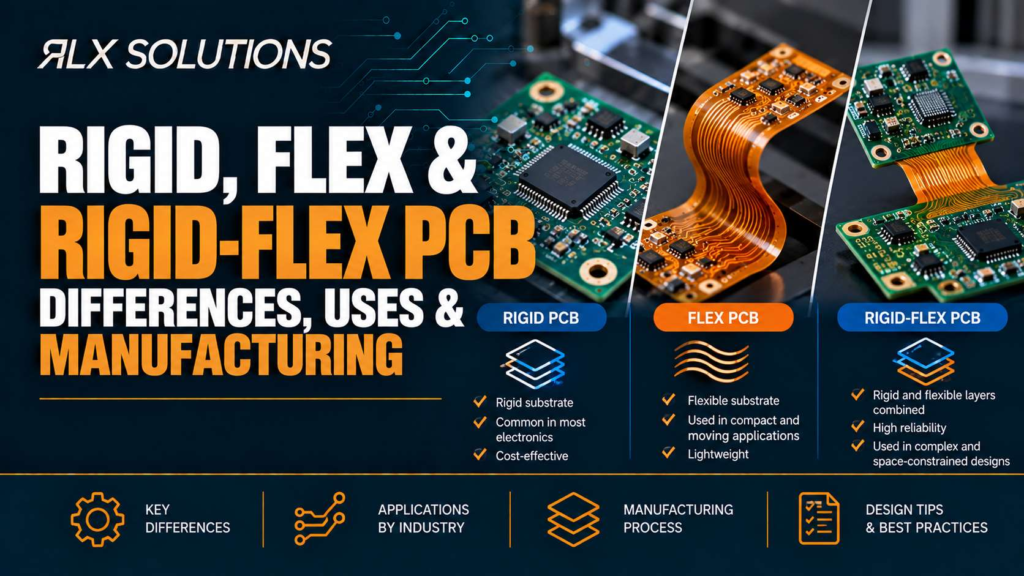
Rigid, flex and rigid-flex PCBs solve different mechanical and electrical packaging problems.
Rigid boards provide a fixed structure, flex circuits bend through constrained spaces, and
rigid-flex combines both in one interconnected construction. RLX Solutions, a contract
electronics manufacturer in Concord, Ontario, evaluates PCB architecture against the
electrical, mechanical and manufacturing requirements of the design.
The distinction matters long before fabrication. Changing from rigid to flex is not simply
a substrate substitution. It changes conductor geometry, bend-zone layout, material behaviour,
panel handling, assembly support and the way mechanical loads reach copper.
Rigid-flex goes further. It replaces connectors or cable assemblies between rigid sections
with integral flexible interconnects. That can reduce interconnect hardware and packaging
volume, but it also makes the layer construction and manufacturing sequence more dependent
on the mechanical design.
Rigid vs Flex vs Rigid-Flex PCB at a Glance
| Decision factor | Rigid PCB | Flex PCB | Rigid-flex PCB |
|---|---|---|---|
| Mechanical form | Fixed planar structure | Bendable circuit | Rigid sections joined by flexible sections |
| Typical design reason | Stable component mounting | Space, motion or folded routing | Integrated 3D electronic packaging |
| Component placement | Usually on rigid board area | Possible, but local mechanical support matters | Usually concentrated on rigid regions |
| Interconnection | Board traces plus connectors or cables where required | Copper traces travel through the flex | Flex layers connect rigid sections directly |
| Bend behaviour | Not intended to bend in service | Can be static or dynamic depending on design | Flex sections provide controlled movement or folding |
| Stackup sensitivity | Driven mainly by electrical and fabrication requirements | Electrical plus mechanical-neutral-axis requirements | Electrical, mechanical and lamination requirements interact |
| Manufacturing impact | Conventional rigid-board process flow | Flexible-material handling and bend-zone control | Multiple material regions and a more involved build sequence |
| Design-change cost | Often localized to the PCB | Can affect bend geometry and enclosure fit | Can affect rigid boards, flex geometry and layer construction together |
A rigid PCB is usually the simplest architecture when the enclosure can accommodate a flat
board and conventional interconnects.
Flex earns its place when the interconnect itself has to bend, fold, move through a hinge
or fit around mechanical obstacles.
Rigid-flex is most useful when separate rigid boards and their interconnecting cables would
otherwise consume space, add connectors or complicate final assembly.
The Structural Difference Changes How Copper Behaves
Rigid PCB conductors are supported by a comparatively stiff laminate system. Flex conductors
operate in a structure intended to deform, which makes strain distribution a first-order
design variable.
When a flex section bends, material on the outside of the bend stretches while material on
the inside compresses. Somewhere between those surfaces is a neutral axis where longitudinal
strain approaches zero. Copper positioned and routed with that behaviour in mind experiences
less cyclic strain than copper placed poorly within the bend construction.
That is why flex routing cannot be treated like ordinary rigid-board routing on a softer sheet.
A trace crossing a bend zone at an angle, a sudden width transition, a via near the bend or
a copper feature that locally stiffens the circuit can concentrate strain. The electrical
drawing may still look correct, but the mechanical loading has changed.
Rigid-flex adds another interface: the transition between a rigid section and the flexible
section. That region needs controlled geometry because the stiffness changes abruptly.
Mechanical load should not be concentrated at the same location as vulnerable copper
transitions, holes or other local discontinuities.
Use Rigid PCBs When Mechanical Stability Is an Asset
A rigid circuit board remains the default choice for a large share of electronics because
it gives components, solder joints and connectors a stable mechanical platform.
It works well when the design can satisfy enclosure, connector and assembly requirements
without requiring the PCB itself to bend.
Rigid construction also leaves the designer with familiar fabrication variables such as
layer count, copper weight, drill geometry, trace spacing, impedance structure and surface
finish. Those variables can still make a rigid board difficult to build, but the board does
not need to perform a second job as a mechanical interconnect.
Consider a hypothetical six-layer, 1.6 mm board carrying a ball grid array (BGA), power stages
and board-to-wire connectors. If the enclosure gives the board enough planar area, keeping the
design rigid avoids adding bend-zone rules and flexible-material interfaces simply to solve
a packaging problem that does not exist.
The more demanding question may instead be via architecture. A 0.20 mm finished through hole
in a 1.6 mm board has an 8:1 thickness-to-hole relationship. Moving to much smaller drilled
holes without changing board thickness pushes the fabrication process harder because plating
must reach reliably through a deeper, narrower barrel.
For dense BGA escape, microvias or via-in-pad may become relevant. Via-in-pad with plated-over
fill uses resin fill, copper capping and planarization so the component pad remains a solderable
surface rather than an open via cavity.
That manufacturing decision is separate from whether the board needs to flex.
Flex PCB Design Starts With the Bend, Not the Outline
A flex circuit should be designed around its mechanical duty before traces are finalized.
There are two fundamentally different conditions. A flex tail may bend once during installation
and then remain stationary, or it may move repeatedly throughout the product’s operating life.
Those two cases impose different fatigue demands even if their finished shapes appear identical.
The bend zone should therefore be treated as functional geometry.
Assume a hypothetical two-layer flex circuit passes through a 180-degree fold inside an enclosure.
One design sends eight parallel traces directly across a 20 mm-long bend region with gradual width
transitions. Another introduces vias and changes trace direction inside that same bend because the
routing was completed before the mechanical fold was defined.
Both may pass an initial electrical continuity test. The second geometry introduces more local
stiffness changes and stress concentration points precisely where copper is being strained.
The likely failure does not begin as an obvious open circuit. Repeated strain can initiate cracking
in copper at a local high-stress location. Electrical resistance may become intermittent before the
conductor separates completely, making the mechanical geometry part of electrical reliability.
Component mass matters for the same reason. A connector or larger package mounted on an unsupported
flexible area can load the copper and solder joints as the circuit moves. Mechanical support,
stiffeners and component placement should therefore be resolved with the enclosure rather than
after routing.
Rigid-Flex Removes Interconnects but Adds Manufacturing Dependency
Rigid-flex PCB construction combines rigid component-bearing sections with integral flexible
interconnect regions.
The benefit is architectural. Instead of using two rigid boards, two connectors and a separate
cable between them, the designer can route the electrical connection through flex layers that
continue between the rigid regions.
That can simplify the finished assembly, especially where boards must sit at different angles
or inside compact three-dimensional packaging.
The trade-off is that formerly independent design decisions become linked. The position of one
rigid section, the flex length between sections, layer usage, bend direction and assembly sequence
now influence one another.
Worked Example: Two 8-Layer Products, Different Cost Drivers
Consider two hypothetical eight-layer electronic assemblies.
| Factor | Board A | Board B |
|---|---|---|
| Layer count | 8 | 8 |
| Architecture | Single rigid PCB | Two rigid regions joined by flex |
| Inter-board connection | External connector and cable | Integral flexible interconnect |
| Component areas | One planar board | Components concentrated on rigid sections |
| Mechanical requirement | Fixed installation | Folded installation |
| Build dependency | Primarily rigid stackup and drilling | Stackup plus rigid-to-flex transitions and flex geometry |
| Assembly impact | Separate cable mating operation | Integrated board must be formed into final position |
Layer count alone therefore does not predict manufacturing effort.
Board A may use complex drilling or controlled impedance, but its physical construction remains
rigid. Board B has the same nominal layer count yet must create both rigid and flexible regions
within a coordinated construction. Material transitions, lamination sequence, mechanical
registration and flex handling become part of the manufacturing problem.
The point is not that eight-layer rigid-flex always costs more by a fixed amount. It is that
quoting by layer count misses the process steps that actually distinguish the builds.
How Manufacturing Changes Across the Three Architectures
Rigid, flex and rigid-flex all begin with an electrical interconnection requirement, but their
manufacturing paths diverge once mechanical behaviour enters the design.
Rigid PCB Manufacturing
A rigid multilayer board is built by creating conductor patterns on individual layers, preparing
inner-layer structures, laminating the stack, drilling holes, metallizing and plating those holes,
imaging outer conductors and applying final protective and surface treatments.
Drilling architecture can change that sequence substantially.
A conventional plated through-hole passes through the finished stack. A buried via connects inner
layers without reaching the outer surfaces. A blind via terminates within the stack. Microvias are
laser-drilled features typically used where routing density demands smaller inter-layer connections.
Blind and buried structures require the manufacturer to create and connect features before the
entire board is fully laminated. That is why two boards with the same layer count can follow
different process routes.
Flex PCB Manufacturing
Flex manufacturing must preserve circuit geometry while working with a construction intended to move.
Material handling becomes more sensitive because thin flexible panels do not behave like rigid sheets
during imaging, registration, drilling and plating. Coverlay or other flexible dielectric structures
also perform the protective function that solder mask provides across much of a rigid board.
Mechanical details remain inseparable from fabrication details. Bend-zone copper, transition geometry,
stiffened areas and component locations all influence whether the fabricated circuit can tolerate
installation and operation.
Rigid-Flex Manufacturing
Rigid-flex combines those process concerns and introduces selective construction.
Some regions must become structurally rigid while others must remain free to bend. The build sequence
must create the required electrical connections without trapping or damaging the flexible portions.
This makes stackup documentation particularly important. Layer identity cannot be ambiguous when some
conductors continue through flexible regions while other layers exist only within rigid sections.
A designer who sends only electrical Gerbers without clearly communicating the intended layer
construction leaves the fabricator to infer mechanical information that should have been controlled
at design release.
Via Architecture Can Decide Whether the Board Is Manufacturable
Vias become more sensitive as routing density increases because they consume both vertical and
horizontal routing resources.
Through holes are efficient when space permits, but they occupy the entire thickness of a multilayer
board even if the electrical connection only needs two nearby layers. Blind, buried and microvia
structures can free routing channels, but they alter the fabrication sequence.
For example, imagine a hypothetical 10-layer board.
One version uses through vias only. Another needs Layer 1 to Layer 2 laser microvias, Layer 2 to
Layer 3 microvias and a buried connection between Layer 3 and Layer 8 to escape a dense BGA field.
Both are 10-layer PCBs. The second board requires a materially different interconnect strategy because
the manufacturer must build those connections into the stack rather than drill every via after final
lamination.
Stacked microvias also place one small via directly above another. Staggered microvias offset the
features laterally. Those geometries affect how loads move through the plated structure and how the
layers are built.
If a BGA uses via-in-pad, filling and capping are adjacent requirements. Leaving a via open in a
solderable pad creates a path that can draw solder away from the intended joint. Filling, planarizing
and capping the feature restores a continuous pad surface for assembly.
Assembly Changes Once the Circuit Board Can Move
Flexibility changes more than bare-board fabrication. It also changes how the assembled circuit is
supported during component placement, soldering, inspection and final integration.
Surface-mount assembly equipment expects controlled board position. A flexible area may therefore
require temporary support or tooling so the populated regions remain stable during printing,
placement and reflow.
Inspection also needs to match the package types being assembled. Solder paste inspection (SPI)
checks deposited paste before reflow. Automated optical inspection (AOI) checks visible post-reflow
conditions. Packages such as BGAs, land grid arrays (LGAs) and quad flat no-lead (QFN) devices can
require X-ray because critical joints are hidden beneath the package.
That becomes especially relevant when a rigid-flex assembly eliminates detachable interconnects.
Once the system is integrated, access for rework may be less convenient than it was with several
independent rigid boards.
Design for assembly should therefore consider how the finished geometry will be held, inspected,
tested and repaired, not just how it fits inside the enclosure.
Surface Finish Still Follows the Assembly Requirement
Board flexibility does not determine surface finish by itself.
The finish should instead match soldering, contact and packaging requirements. Common options across
PCB manufacturing include hot air solder levelling (HASL), electroless nickel immersion gold (ENIG),
electroless nickel electroless palladium immersion gold (ENEPIG), immersion silver, immersion tin and
organic solderability preservative (OSP).
The manufacturing consequence appears at the interface between the bare board and assembly process.
A fine-pitch surface-mount pad benefits from predictable planarity. A connector contact may impose
different wear or mating requirements. A wire-bonding application creates another surface requirement.
Choosing a board architecture first and blindly copying the finish from a previous project treats
two separate engineering decisions as though they were one.
Choose the Architecture From the Mechanical Constraint Backward
Start with rigid unless the product gives you a specific reason not to.
Choose a rigid PCB when the electronics fit on a stable planar structure and connectors or cables
do not create an unacceptable packaging, reliability or assembly problem.
Choose flex when the circuit itself needs to pass through a constrained path, fold during installation
or accommodate controlled movement. Define bend regions and mechanical support before final routing.
Choose rigid-flex when several rigid component regions need to occupy different planes and integrating
their interconnection provides enough system value to justify a more dependent stackup and manufacturing
sequence.
The deciding calculation should be made at system level. A separate cable assembly has connectors,
mating operations, space claims and possible service advantages. Rigid-flex removes some of those
interfaces but combines more of the product into one manufactured structure.
That trade should be made deliberately rather than reducing the decision to bare-board unit price.
Send the Stackup With the Mechanical Intent
A manufacturer needs enough information to distinguish electrical connectivity from physical
construction. Fabrication data should therefore be accompanied by the intended stackup, drill
information, impedance requirements and fabrication notes where relevant. Assembly projects also
need the bill of materials, centroid data and assembly documentation.
If you are preparing a rigid PCB or evaluating a more mechanically integrated architecture, RLX can
review the manufacturable portions of the design as part of an engineer-reviewed DFM process. Send the
fabrication and assembly package with the mechanical requirements clearly identified so those
constraints are visible before production decisions are locked.
FAQ
Is rigid-flex the same as connecting two rigid PCBs with a flex cable?
No. A cable or separate flex circuit creates discrete interconnect interfaces between independently
manufactured items. A rigid-flex PCB incorporates rigid and flexible regions into one circuit
construction. The finished products can serve a similar packaging purpose, but their stackup,
manufacturing sequence, assembly flow, repair strategy and connector count can be very different.
Can components be mounted directly on a flex PCB?
Yes, but the mechanical behaviour around the component matters. Packages, connectors and solder joints
should not be placed where repeated bending transfers damaging strain into their terminations. Stiffened
component areas and controlled transition geometry are commonly used so the local assembly behaves
predictably while other regions remain flexible.
Do flex circuits use the same routing rules as rigid PCBs?
Not completely. Electrical constraints still apply, but a flex circuit adds mechanical strain to the
routing problem. Trace direction through bends, width transitions, copper distribution, vias and nearby
stiffened regions can all affect fatigue behaviour. The bend geometry should therefore be defined before
routing is treated as finished.
Are rigid-flex boards always better than connectors and cables?
No. Rigid-flex can reduce separate interconnects and help fit electronics into compact three-dimensional
spaces, but it also couples the mechanical design more tightly to the PCB stackup. Connectors and cable
assemblies can offer modularity, replacement access and easier separation of subassemblies. The better
architecture follows the product’s packaging, service and reliability requirements.
What files should I send for a PCB manufacturing review?
For fabrication, useful manufacturing files include Gerber RS-274X, ODB++ or IPC-2581 data with NC
drill files, plus the stackup, impedance targets and fabrication notes where applicable. Assembly work
also requires the bill of materials, pick-and-place or centroid file and assembly drawing so fabrication
and component placement requirements can be reviewed together.