Rigid-flex PCB design guidelines start with one rule: treat the flex region as a mechanical structure, not simply another PCB layer. Bend geometry, copper direction, layer transitions, vias and component placement all affect reliability. RLX Solutions, a contract electronics manufacturer in Concord, Ontario, reviews these interactions during engineer-reviewed design for manufacturability (DFM).
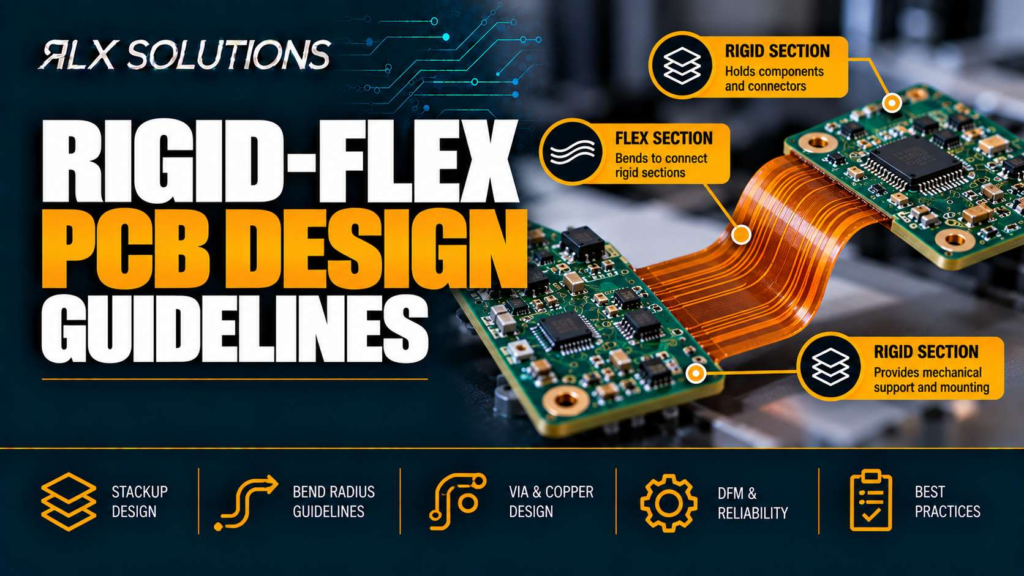
A rigid-flex printed circuit board combines rigid circuit board sections with flexible circuitry in one interconnected structure. That integration can remove connectors and cable assemblies, reduce packaging volume and control how an interconnect folds into the enclosure. It also makes the PCB stackup part of the mechanical design.
The layout therefore cannot be finished first and made flexible later. Mechanical motion, stackup construction, copper geometry, impedance requirements and assembly constraints have to converge before manufacturing data is released.
Start the rigid-flex stackup with the mechanical architecture
Define where the circuit board must remain rigid, where it must flex and how those regions meet before routing dense circuitry.
A rigid-flex stackup is not uniform across the complete board outline. Rigid areas contain the layers and structural material needed for components and interconnection. Flex areas continue selected conductive layers through regions intended to bend or fold. That change in construction creates transition zones that deserve explicit design attention.
Your fabrication documentation should make the intended construction unambiguous. At minimum, the manufacturer needs to understand the layer sequence, which layers continue through each flex region, finished geometry and the boundaries between rigid and flexible sections.
Consider a hypothetical 8-layer board. Layers 1 through 8 exist in the rigid sections, but only Layers 4 and 5 continue through a flexible arm joining two rigid islands. Routing a signal from Layer 1 to Layer 6 in the rigid area is fundamentally different from expecting those layers to continue through the arm. The electrical topology must match the physical stackup.
This is also why layer count alone says little about manufacturing difficulty. Two 8-layer designs can require very different process sequences depending on how their flex layers, vias and rigid sections interact.
Keep the flex section as simple as the electrical design allows
Every additional conductive or structural layer in a bend region changes its mechanical behaviour. More material increases thickness and shifts strain through the stack.
If a flex section only needs to carry a defined set of signals and power connections between rigid islands, avoid extending layers into it without an electrical or mechanical reason. The question is not whether another layer fits in the CAD stackup. The question is what that layer does when the assembly bends.
Design bend zones before placing vias and components
The bend zone is the region intended to absorb mechanical deformation. Features that concentrate stress should stay outside it unless the construction has been specifically engineered around them.
Vias, pads, component terminations and abrupt copper geometry can create local stiffness changes. A bend that repeatedly loads those discontinuities can concentrate strain instead of distributing it along the flexible section.
The same concern applies at the rigid-to-flex transition. Copper enters an area with different mechanical support, so abrupt geometry or poorly positioned features can create a local stress concentration.
For a hypothetical design, suppose a flex tail is 12 mm wide and must make a 90-degree fold between two rigid sections. Placing a row of vias directly where the fold begins creates a very different mechanical condition from moving the via field into the rigid area and allowing uninterrupted traces to pass through the bend.
The second layout gives the copper a continuous region in which to deform. The first asks the bend to occur around plated structures and geometry changes.
Static and dynamic flex are different design problems
A static-flex application is bent into position during assembly and then experiences little intentional movement. A dynamic-flex application repeatedly bends during operation.
That distinction should be captured in the mechanical requirements before routing starts. A fold used once to package a display module does not impose the same fatigue problem as a flexible interconnect that moves whenever a mechanism cycles.
For dynamic movement, the number of flex layers, copper geometry and bend path become particularly significant because the conductors experience repeated strain. Routing choices that survive one installation fold may perform differently after repeated mechanical cycling.
Route copper through bend zones with mechanical strain in mind
Copper routing in a flex region should distribute mechanical strain rather than create sharp local concentrations.
Keep traces smooth through the bend. Avoid abrupt directional changes and unnecessary width transitions where the circuit is expected to flex. Where traces must change direction, gradual geometry is mechanically preferable to routing that introduces a sharp corner into the highest-strain region.
Trace orientation matters as well. A conductor running through a bend experiences a different strain pattern from copper geometry that creates a local stiff point across the bend.
The effect becomes easier to see with a simple hypothetical geometry. Imagine a 20 mm-long flex section carrying eight signals between rigid boards. Routing those eight traces as continuous conductors through the flex area produces a relatively uniform copper pattern. Adding unused copper islands, via pads and repeated width changes inside the same 20 mm section changes how stiffness is distributed.
The electrical connectivity may be identical. The mechanical structure is not.
Balance electrical needs against copper distribution
Removing copper indiscriminately is not the objective. Power distribution, shielding, electromagnetic compatibility and controlled impedance can all require reference conductors.
Instead, identify what each copper feature is doing. A plane needed as the return path for a high-speed interface has an electrical function. A large copper feature left in a bend zone simply because it existed in the rigid-board layout may not.
Rigid-flex design forces electrical and mechanical decisions into the same geometry. Neither discipline can be treated as an afterthought.
Keep vias out of flex regions unless the construction requires them
A plated through-hole via is a drilled and plated structure. A microvia is a laser-drilled interconnection used to connect selected layers over a much shorter vertical distance. Both introduce geometry that must be considered against the actual layer construction.
Where possible, complete layer transitions in a rigid region before traces enter the flex section. That leaves the bend region carrying continuous copper rather than drilled interconnections.
Via architecture also changes the fabrication sequence. Blind vias connect an outer layer to selected internal layers and require sequential lamination in multilayer constructions. Buried vias connect internal layer pairs. Stacked or staggered microvias add further dependencies between drilling, plating, filling and lamination.
Via-in-pad plated over fill (POFV) adds another adjacent process. The via is resin filled, copper capped and planarized so the finished pad can support component attachment without leaving an open via in the land.
Those processes may solve a routing-density problem in a rigid section, but they should be chosen because the component escape or interconnection architecture requires them.
Check aspect ratio before freezing the drill table
Aspect ratio links hole geometry to the thickness through which the hole must be formed and plated. A via that looks ordinary in plan view can become difficult because of the vertical geometry.
Suppose a hypothetical rigid section is 1.6 mm thick and uses a 0.20 mm drilled hole. Dividing thickness by hole diameter gives an 8:1 geometry. If another revision keeps the same hole but increases the relevant drilled thickness to 2.0 mm, the geometry becomes 10:1.
Nothing changed on the XY view of the layout. The manufacturing condition changed substantially in the Z-axis.
That is why rigid-flex DFM must examine the stackup and drill architecture together.
Controlled impedance must survive the rigid-to-flex transition
Controlled impedance depends on conductor geometry and its relationship to reference conductors and dielectric material. When those relationships change, the transmission structure changes.
A high-speed trace may therefore have one geometry in a rigid section and another through the flexible portion. Copying the same trace width across both regions does not by itself preserve the same impedance.
Start with the electrical requirement, then develop the stackup and trace geometry around it. The fabrication package should identify the impedance target and the traces or structures to which it applies.
For a hypothetical USB differential pair, imagine the signals begin on Layer 3 of an 8-layer rigid section but continue on one of two conductive flex layers through a 30 mm flex arm. The reference structure and dielectric geometry have changed. The flex portion needs to be treated as its own transmission-line geometry rather than as a visual continuation of the rigid Layer 3 route.
The failure may not appear as an open or short. Instead, the assembled product can show signal-integrity degradation even though basic continuity testing passes.
This is where fabrication verification matters. Controlled-impedance requirements should be established before the stackup is locked, with test structures and time-domain reflectometry (TDR) used where specified for manufacturing verification.
Board A and Board B show why layer count does not predict cost
Consider two hypothetical 10-layer rigid-flex circuit boards with the same overall outline and component set.
| Decision factor | Board A | Board B |
|---|---|---|
| Layer count | 10 layers | 10 layers |
| Flex connection | Two conductive layers continue between rigid sections | Two conductive layers continue between rigid sections |
| Rigid-area vias | Through vias | Blind and buried via structure |
| Microvias | None | Layer 1 to Layer 2 and Layer 2 to Layer 3 |
| Internal connection | Through-hole structure | Buried connection between Layer 3 and Layer 8 |
| Component escape | Conventional fanout | Dense via-in-pad fanout |
| Lamination dependency | Simpler interconnection sequence | Multiple structures depend on build sequence |
| Main cost driver | Base rigid-flex construction | Additional drilling, filling, plating and lamination operations |
Both boards are 10 layers, but Board B creates more manufacturing dependencies.
Its Layer 1 to Layer 2 and Layer 2 to Layer 3 microvias must fit the lamination sequence. The buried Layer 3 to Layer 8 connection introduces another vertical interconnect requirement. If via-in-pad is used beneath fine-pitch components, filling, capping and planarization become part of the pad construction.
Board A avoids those operations because its routing can be completed with through vias in the rigid regions.
This is why a quote based primarily on layer count can hide the real cost mechanism. Process sequence, via architecture and flex construction matter at least as much as the number printed beside “layers” in the specification.
Component placement has to respect both bending and assembly
Components belong on mechanically supported regions unless the design has been engineered for another arrangement. The assembly process also needs access, stable support and suitable fiducial and tooling geometry.
Rigid-flex creates an additional question: what shape is the product during assembly?
A circuit board may be fabricated flat but folded later into the enclosure. That means the manufacturing panel, component-placement sequence, inspection access and final mechanical configuration are different states of the same product.
The assembly drawing should make those states clear.
Fine-pitch devices add another interaction. A ball grid array (BGA), land grid array (LGA) or quad-flat no-lead (QFN) package may require X-ray inspection because solder joints are hidden from direct optical inspection. Dense BGA fanout may also drive microvias or via-in-pad construction, which then feeds back into the bare-board fabrication sequence.
A 0.5 mm-pitch BGA on a rigid island, for example, may fit easily in the mechanical outline but force a different escape architecture from a larger-pitch device. Moving the package a few millimetres away from the rigid-to-flex transition can also create more room to complete via transitions before signals enter the flex region.
Placement is therefore a fabrication, assembly and mechanical decision at the same time.
Define the fabrication package so the flex intent cannot be misread
Rigid-flex manufacturing data needs more than copper artwork. The manufacturer has to reconstruct the intended physical object from the files you release.
- Layer stackup. Show the complete layer order and identify which conductive layers continue through each flexible section.
- Rigid and flex boundaries. Make the transitions explicit rather than expecting them to be inferred from routing.
- Mechanical geometry. Include the board outline, flex shape and dimensional requirements needed to interpret the finished structure.
- Drill information. Separate through, blind, buried and laser-drilled structures where applicable.
- Impedance requirements. Identify target structures and include the impedance information needed for stackup engineering.
- Assembly information. Provide the bill of materials (BOM), pick-and-place data and assembly drawing for populated builds.
- Special notes. State requirements that cannot be represented reliably by Gerber geometry alone.
Gerber RS-274X, ODB++ and IPC-2581 can carry manufacturing information in different ways, but the file format does not replace clear design intent.
A technically valid data set can still generate questions if the stackup drawing and fabrication notes contradict the artwork. Resolve those conflicts before release rather than forcing manufacturing engineering to decide which file governs.
Run DFM before the rigid-flex geometry becomes expensive to change
Rigid-flex DFM should happen while the mechanical and electrical architecture can still move.
The highest-value review is not a final search for obvious spacing violations. It checks whether the chosen stackup, via architecture, flex geometry, impedance requirements, assembly plan and manufacturing sequence agree with each other.
A practical pre-release review should examine these conditions:
- Bend regions are identified and kept free of avoidable stress-concentrating features.
- Copper geometry through flexible regions matches the intended mechanical behaviour.
- Layer transitions occur in mechanically appropriate locations.
- Blind, buried and microvia structures agree with the lamination sequence.
- Via aspect ratios are evaluated against the actual drilled thickness.
- Controlled-impedance structures are defined for both rigid and flexible regions.
- Component placement leaves workable routing and manufacturing transitions.
- Fabrication and assembly documentation describe the same physical product.
Finding a conflict here is cheaper than finding it after tooling, lamination planning or assembly preparation has begun.
A common example is a late mechanical revision that shortens a flex arm. Electrically, every net may still connect. Mechanically, the new geometry may move the intended bend onto a via field or rigid-to-flex transition. DFM has to catch the consequence of the dimensional change, not merely confirm connectivity.
Treat rigid-flex as one electromechanical system
The strongest rigid-flex designs are developed from three models at once: electrical connectivity, manufacturing construction and mechanical movement.
Changing one model should trigger a review of the other two. Moving a BGA can change via architecture. Changing via architecture can change lamination. Changing the stackup can alter impedance. Shortening a flex section can move the bend into a copper or via transition.
That dependency chain is the defining design problem.
For engineers preparing a rigid-flex design for quotation or production review, RLX can review the board data and manufacturing requirements as part of the quotation process. Send the fabrication package and, for assembled boards, the BOM, pick-and-place data and assembly drawing so the electrical and manufacturing assumptions can be reviewed together.
Frequently Asked Questions
What files should I prepare for a rigid-flex PCB manufacturing review?
Prepare complete fabrication data rather than copper layers alone. Manufacturing files can include Gerber RS-274X, ODB++ or IPC-2581 plus NC drill data, a stackup drawing, impedance targets and fabrication notes. For assembled circuit boards, add the BOM, pick-and-place or centroid file and assembly drawing so fabrication and component-placement requirements can be reviewed together.
Why should vias be moved away from a rigid-flex bend area?
A via changes the local copper and structural geometry exactly where the circuit may need to deform. Moving layer transitions into a supported rigid region can leave continuous traces through the bend and reduce abrupt stiffness changes. The exact layout still has to be evaluated against the intended flex construction and mechanical motion.
Can controlled-impedance signals cross from rigid PCB sections into flex?
Yes, but the flex section must be treated as a transmission-line structure rather than assuming the rigid-board trace geometry can simply continue unchanged. Changes in dielectric geometry, reference conductors and copper construction can change impedance. Define the electrical target early enough for the rigid and flexible stackups to be engineered around it.
When do microvias become useful in a rigid-flex design?
Microvias become relevant when routing density or component escape cannot be handled efficiently with conventional drilled interconnections. For example, a dense BGA on a rigid section may drive short layer-to-layer connections. That decision affects drilling, plating, filling and potentially lamination, so microvia architecture should be resolved with the stackup rather than added after routing.
How does rigid-flex design affect PCB assembly inspection?
Rigid-flex changes mechanical support and access during assembly, while the component package determines the inspection method. Hidden solder joints beneath BGA, LGA and QFN packages can require X-ray inspection. The assembly plan should therefore consider the board’s flat manufacturing state, component locations and its final folded configuration before production documentation is released.