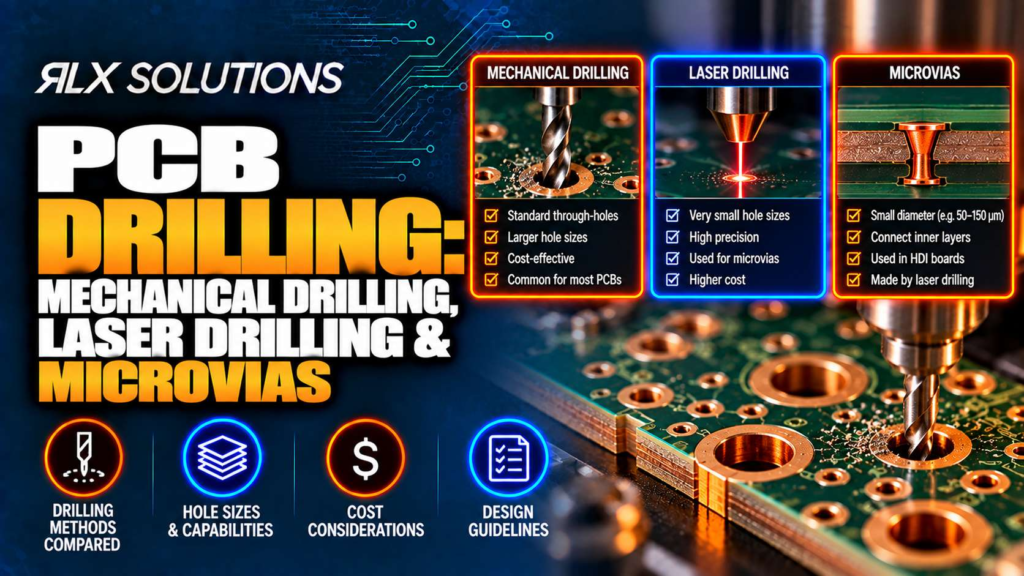
PCB drilling method follows the interconnect geometry, not simply the layer count. Mechanical drilling suits plated through-holes and larger features, while laser drilling creates the small blind microvias used in high-density interconnect (HDI) structures. RLX Solutions, a contract electronics manufacturer in Concord, Ontario, reviews via architecture against the proposed stackup before a board is quoted.
Mechanical and laser drilling solve different interconnect problems
A drilled hole becomes part of the electrical and mechanical structure of a printed circuit board once it is cleaned, metallized and plated. Choosing the drilling process therefore affects more than hole diameter. It influences pad size, routing density, layer transitions, lamination sequence and the difficulty of producing a continuous plated connection. Learn more about bare PCB fabrication and multilayer stackups.
Mechanical drilling removes laminate and copper with a physical cutting tool. It is the natural process for holes that pass through a conventional stackup, including plated through-holes (PTHs), non-plated mounting holes and many larger vias. For the full picture, see our PCB Manufacturing Guide.
Laser drilling removes material without a mechanical cutting tool and is primarily used to form small, depth-controlled connections through thin dielectric layers. That makes it suited to microvias and HDI build-up structures.
A microvia is a small via used to make a short layer-to-layer connection in a dense interconnect structure. Its value is not simply that the hole is small. A microvia can free routing area that would otherwise be consumed by a larger drilled hole, pad and clearance through multiple layers.
| Decision factor | Mechanical drilling | Laser drilling |
|---|---|---|
| Primary use | Through-holes, larger vias, mounting and component holes | Microvias and dense blind interconnects |
| Material removal | Physical cutting | Localized ablation |
| Connection depth | Commonly through the stack | Commonly across a thin dielectric |
| Routing impact | Hole and clearance can occupy many layers | Connection can terminate at a selected layer |
| HDI role | Useful for through and internal structures | Enables small build-up microvias |
| Main design constraint | Drill diameter and aspect ratio | Microvia geometry, layer sequence and stackup |
| Related processes | Desmear, metallization and plating | Sequential lamination, plating, filling and capping where required |
The important distinction is architectural. Replacing a mechanically drilled via with a laser-drilled microvia can change which layers are connected and which layers remain available for routing.
Mechanical PCB drilling starts with diameter and aspect ratio
For a mechanically drilled PTH, the bit passes through the material stack and creates the hole that will later receive conductive plating. The drill has to remain stable through that depth while producing a hole suitable for subsequent cleaning and metallization.
Aspect ratio describes hole depth relative to hole diameter. As a mechanical hole becomes smaller or the board becomes thicker, its aspect ratio increases. That matters because fabrication does not end when the drill exits the panel. The hole wall still needs to be processed and plated consistently through its depth.
The fabrication range includes mechanical PTH drilling down to 0.15 mm, with a standard maximum aspect ratio of 10:1 and 12:1 subject to review. Mechanical drill sizes extend to 6.5 mm. Hole tolerance is ±0.08 mm for plated holes and ±0.05 mm for non-plated holes.
Consider a hypothetical 1.6 mm-thick, 8-layer circuit board using a 0.20 mm finished through-via geometry. The depth-to-diameter relationship is 1.6 ÷ 0.20, or 8:1. If the same board thickness is retained while the hole is reduced to 0.15 mm, that ratio becomes roughly 10.7:1.
Nothing changed in the layer count, yet the smaller hole moved the design into a more demanding manufacturing condition. This is why specifying the smallest possible drill everywhere can be counterproductive. A few hundred microns saved at the via may impose a harder drilling and plating problem through the entire stack.
Annular ring also enters the calculation. The annular ring is the copper surrounding a drilled hole on the connected layer. The fabrication geometry supports a minimum annular ring of 0.075 mm on inner layers and 0.1 mm on outer layers. Drill size, pad size and registration therefore have to be considered together rather than as independent design-rule entries.
Laser drilling changes the layer connection, not just the hole size
Laser drilling becomes useful when the required interconnect is too small or too localized for a conventional through-hole architecture. The fabrication range includes laser-drilled microvias down to 0.10 mm, including stacked and staggered structures that are confirmed against the proposed HDI stackup.
A laser-drilled microvia typically connects layers across a much shorter vertical distance than a through-hole. Instead of creating a barrel through every layer, the process removes material in a local build-up layer so the resulting via can connect selected conductors.
That difference has a direct routing consequence.
Suppose a 10-layer PCB needs a connection from Layer 1 to Layer 2 beneath a dense component. A mechanically drilled through-via used for that connection would physically pass through the full stack, even if the signal only needs to reach Layer 2. Its pads and clearances can restrict routing farther down the board.
A Layer 1 to Layer 2 microvia terminates after making the required connection. Layers below it are not occupied by the same through-barrel. That can release routing channels on inner layers and make a dense escape pattern possible without automatically adding more layers.
The trade-off is process sequence. Once vias terminate at specific internal layers, the manufacturer must build the interconnect structure in stages. The drill file alone no longer tells the full manufacturing story.
Microvias make the stackup part of the drill definition
A conventional through-via can be described largely by its location, diameter and plating requirement. A microvia needs another piece of information: the layers it connects.
Layer 1 to Layer 2 and Layer 2 to Layer 3 microvias may share the same nominal diameter, but they are not interchangeable manufacturing features. They exist at different points in the build sequence.
This is where sequential lamination enters the design. Sequential lamination builds portions of a multilayer PCB in stages so blind or buried connections can be formed before later layers make those features inaccessible.
A buried via is an interconnect between inner layers that does not reach either external surface. A blind via starts at an outer surface and terminates on an inner layer. Both alter the sequence in which drilling, plating and lamination occur.
Consider an 8-layer design with a buried connection from Layer 3 to Layer 6 plus a Layer 1 to Layer 2 microvia. The internal Layer 3 to Layer 6 structure must exist at a stage when those layers can still be drilled and processed. The Layer 1 to Layer 2 connection belongs to a later build-up stage.
The designer sees one finished 8-layer board. Manufacturing sees multiple interdependent structures that must be completed in the correct order.
That distinction is a major reason two PCBs with identical dimensions and layer counts can carry different fabrication cost.
Same 10 layers, very different drilling cost
Consider two hypothetical boards with the same outline, material family and 10-layer count.
| Decision factor | Board A | Board B |
|---|---|---|
| Layer count | 10 | 10 |
| Board thickness | 1.6 mm | 1.6 mm |
| Main via architecture | 0.20 mm mechanical through-vias | Mixed through-vias and 0.10 mm microvias |
| Blind structure | None | Layer 1 to 2 and Layer 10 to 9 |
| Internal structure | None | Buried via between Layer 3 and Layer 8 |
| Via-in-pad | No | Used in dense component region |
| Lamination structure | Conventional multilayer build | Sequential build required |
| Manufacturing burden | Mechanical drilling and through-hole processing | Multiple via structures, additional build stages, filling and capping where specified |
Board B does not cost more because “10-layer HDI” is inherently expensive. The mechanism is more specific.
Its layer-selective vias require manufacturing operations at different stages of the stackup. The buried structure must be formed before it disappears inside later laminations. Outer microvias are created after their relevant build-up layers exist. Via-in-pad structures can add resin filling, copper capping and planarization.
Every added dependency creates another place where registration, plating or lamination has to remain controlled before the next operation can begin.
Board A avoids those dependencies. If its routing can be completed with mechanically drilled through-vias, adding laser-drilled structures would introduce process work without solving a design problem.
That is the useful cost rule: use HDI interconnects where they recover routing area or enable the required package escape, rather than making every via smaller by default.
Stacked and staggered microvias change the manufacturing sequence again
One microvia can connect adjacent build-up layers. Moving vertically through several layers may require multiple microvias.
A stacked microvia structure places those vias vertically over one another. A staggered structure offsets successive vias instead.
The distinction affects both routing and fabrication. Stacking preserves a compact XY footprint, which can matter beneath dense ball grid array (BGA) regions. It also creates a vertical structure in which the next via depends on the material and processing beneath it.
Imagine a 12-layer board where a signal must move from Layer 1 to Layer 3 inside a tightly constrained fanout region.
One option uses a Layer 1 to Layer 2 microvia directly above a Layer 2 to Layer 3 microvia. That is a stacked structure. Another moves the Layer 2 to Layer 3 microvia sideways from the first landing location. That is staggered.
The stacked version consumes less lateral routing area. The staggered version consumes additional XY space but changes the physical relationship between the two vias.
Neither structure should be selected from a generic “microvia” rule in the CAD library. The actual stackup, dielectric construction, pad geometry, filling requirement and build sequence need to agree with the via architecture.
Via-in-pad adds fill, cap and planarization to drilling
Via-in-pad places a via within a component land rather than beside it. It is useful when conventional dog-bone fanout consumes too much room or when dense BGA geometry leaves insufficient space for a separate via and connecting trace.
The hole, however, cannot be treated like an ordinary open via beneath a solderable pad.
Plated over filled via (POFV) construction fills the via with resin, adds a copper cap and planarizes the surface. The goal is to restore a suitable pad surface while retaining the electrical path through the via.
This is directly adjacent to laser drilling because dense microvia fanout frequently pushes the designer toward via-in-pad. Specifying the hole without specifying the pad treatment leaves an important manufacturing requirement unresolved.
For example, consider a 6-layer board with a dense BGA region. A 0.10 mm Layer 1 to Layer 2 microvia placed inside the land may release the routing channel that a separate via would occupy. Once that choice is made, the fabrication package must communicate the via structure and fill requirement clearly enough that the pad is processed as intended.
Via-in-pad fabrication can use resin fill, copper cap and planarization on 4-layer and higher stackups. Button plating is another available process for BGA fanout and density optimization.
The drilling decision has therefore expanded into a pad-finishing decision. That is exactly the kind of adjacent process that can be missed when the layout team focuses only on whether the hole fits.
Blind and buried vias need a layer-pair map
Blind and buried vias are easiest to review when the design documentation treats them as explicit layer pairs rather than one generic drill category.
A useful fabrication definition distinguishes structures such as:
- Through-via, Layer 1 to Layer 10
- Blind via, Layer 1 to Layer 2
- Blind via, Layer 10 to Layer 9
- Buried via, Layer 3 to Layer 8
- Stacked microvia, Layer 1 to Layer 2 over Layer 2 to Layer 3
That mapping exposes the manufacturing sequence before fabrication starts. It also lets the engineer see whether multiple special via structures are solving genuine routing constraints or simply accumulating through local layout decisions.
Buried vias can be formed between inner layer pairs on 4-layer and higher stackups. Blind vias similarly require sequential lamination on multilayer builds. Once either appears in the design, the stackup and drilling architecture need to be reviewed as one system.
Design the via architecture before routing locks it in
The most expensive time to discover a drilling problem is after dense routing has made every via location dependent on surrounding traces.
Start with the package escape and stackup. Identify which signals truly need layer-selective transitions, then reserve mechanical through-vias for connections that do not benefit from HDI geometry.
The fabrication package should make several items unambiguous:
- Finished board thickness and stackup. Aspect ratio and layer-specific drilling cannot be evaluated without vertical geometry.
- Drill data. NC drill files define hole locations and sizes, but blind, buried and microvia structures also need clear layer-pair identification.
- Via treatment. State which vias are filled, capped or used in pads rather than expecting the manufacturer to infer intent from placement.
- Impedance targets where applicable. Via transitions interact with high-speed routing, while controlled impedance requirements also affect the surrounding stackup.
- Fabrication notes. Separate electrical vias from non-plated mechanical holes, slots and other drilled features.
- Native design or manufacturing data where available. Gerber RS-274X, ODB++, IPC-2581 and NC drill are accepted manufacturing formats, while a stackup PDF and impedance targets provide additional fabrication context.
This information gives an engineer-reviewed design for manufacturability (DFM) review enough context to examine the hole geometry as part of the complete board rather than checking drill diameters in isolation.
Do not separate drilling from plating and inspection
A hole is not a useful interconnect merely because its geometry was drilled correctly. It must survive the processes that turn the exposed hole into a conductive connection.
For a plated structure, that means the hole condition and metallization have to support continuous copper through the intended connection. High aspect ratio through-holes make that task more demanding because plating must reach along a deeper, narrower barrel.
Microvias create a different geometry, but they introduce their own dependencies around cleaning, metallization, filling and capping. Stacked structures add further dependence between one completed via and the next layer transition above it.
Performance class also matters. IPC-6012 Class 3 fabrication applies tighter annular-ring and plating requirements than Class 2, with cross-section sampling used for high-reliability builds. That does not change the basic physics of drilling, but it changes how much margin the fabrication geometry must preserve and how the finished structure is evaluated.
The design implication is simple: do not spend all available tolerance on routing density before fabrication review. A CAD layout can be geometrically valid while leaving little manufacturing margin around the drilled and plated structure.
Choose the simplest drilling method that solves the routing problem
Mechanical drilling should remain the default where a conventional through-hole architecture provides enough routing density. It handles plated through-holes across all supported layer counts and avoids adding sequential build stages simply to make a via smaller.
Laser-drilled microvias become useful when their short, small layer transitions create a concrete layout advantage. Fine-pitch fanout, via-in-pad geometry and the need to preserve routing channels on deeper layers are typical reasons.
Blind or buried structures make sense when terminating the via on selected layers releases enough routing area to justify the changed build sequence.
Stacked microvias deserve another level of scrutiny because several vertical transitions become dependent on one another. If a staggered structure or different breakout strategy fits the available space, that alternative should be compared before the stackup is frozen.
The decision should therefore move in this order: package escape, routing density, layer transitions, stackup, via architecture, then drill technology. Starting with “laser or mechanical?” reverses the engineering problem.
Get the drill architecture reviewed with the stackup
If you are specifying mechanical vias, blind or buried structures, microvias or via-in-pad on a board heading into fabrication, RLX reviews the geometry and stackup as part of every quote. Send the complete manufacturing files so the drilling method, aspect ratio, layer pairs and related fabrication requirements can be checked before production.
Frequently Asked Questions
What is the minimum PCB drill size?
For fabrication, the minimum mechanical drill for a plated through-hole is 0.15 mm. Laser-drilled microvias can go to 0.10 mm. The diameter alone does not establish manufacturability because board thickness, aspect ratio, annular ring, layer pair and via treatment can change the process required.
Can a microvia be placed directly in a BGA pad?
Yes. Via-in-pad can be used for dense BGA fanout, but the fabrication treatment matters. Plated over filled via construction uses resin filling, copper capping and planarization to produce the required pad surface. Via-in-pad is available on 4-layer and higher stackups and should be defined explicitly in the fabrication data.
What is the maximum aspect ratio for a mechanically drilled PCB via?
The standard maximum aspect ratio is 10:1, with 12:1 available subject to the actual build. Aspect ratio is the relationship between hole depth and diameter, so reducing drill diameter or increasing board thickness pushes the geometry upward even when the layer count stays unchanged.
Are blind and buried vias the same as microvias?
No. Blind and buried describe where a via begins and ends in the stackup. A blind via reaches an external surface, while a buried via remains between inner layers. A microvia describes a small interconnect structure commonly associated with HDI construction. The terms can overlap, but they describe different properties of the interconnect.
What files are needed to review PCB drilling?
Manufacturing data can include Gerber RS-274X, ODB++, IPC-2581 and NC drill files. A stackup PDF, fabrication notes and impedance targets provide additional context. For blind, buried or microvia designs, the intended layer pairs and any filling or capping requirements should also be unambiguous so the drill architecture can be reviewed against the build sequence.
Does IPC Class 3 change PCB drilling requirements?
IPC-6012 Class 3 fabrication applies tighter annular-ring and plating criteria than Class 2. For the designer, that makes manufacturing margin around drilled and plated structures more significant. Class 3 builds also involve cross-section sampling. The drilling geometry should therefore be reviewed together with plating, registration and the complete stackup rather than treated as an isolated drill-table decision.