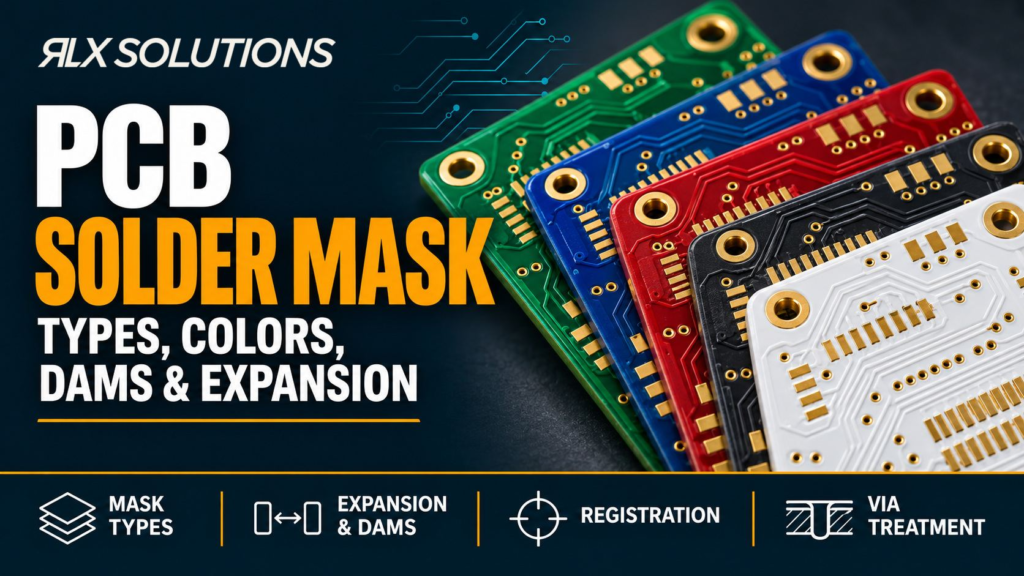
Solder mask is the cured insulating coating that covers most exposed copper on a printed circuit board while leaving pads and selected features open for soldering, test, contact or plating. Its geometry matters because pad openings, registration and narrow dams directly affect fabrication margin and the assembly process.
RLX Solutions, a contract electronics manufacturer based in Concord (Vaughan), Ontario, reviews mask data as part of bare-board fabrication with mask opening and dam review, so the released openings, dams and via treatment can be checked against the actual circuit board geometry before fabrication.
What the Coating Actually Controls on a PCB
The green, black, blue or other colored layer on a bare PCB is not simply a protective finish. It defines where copper stays covered and where copper must remain exposed. That makes it part of both fabrication and assembly.
The coating performs three practical jobs. First, it isolates traces and planes from direct contact, contamination and accidental solder wetting. Second, it creates openings around component pads, test points, connector contacts and other features that must remain accessible. Third, it can leave narrow strips of material between adjacent openings. Those strips are solder dams, also called mask webs or slivers.
A solder dam does not replace good pad spacing or stencil design. Its job is to create a physical boundary between nearby exposed copper areas. During reflow or hand soldering, that boundary can reduce the tendency for molten solder to spread from one pad to the next.
This geometry is created from the top and bottom mask layers in the fabrication data. The manufacturer uses those layers with the copper artwork, drill data and fabrication notes. If the mask layer and copper layer disagree, the problem is not cosmetic. A pad can become partly covered, a thin web can disappear, or copper that should stay protected can be exposed.
The full fabrication sequence matters here. The RLX overview of each fabrication step from imaging to final verification covers the broader imaging, drilling, plating, etching, mask, finish and verification flow; this article focuses specifically on the coating geometry and the design decisions around it.
Solder Mask Types and Where Each Fits
Several mask systems exist in PCB fabrication, but they do not create the same resolution or process control.
Liquid photoimageable mask, or LPI, is a liquid coating that is applied over the board, imaged through artwork or direct imaging, developed to remove material from required openings, then fully cured. Because the opening pattern is created photographically, LPI is well suited to dense modern circuit boards where pad clearance and dam width must be controlled closely.
Dry-film photoimageable mask uses a photosensitive film laminated onto the board. It can produce defined features, but the film structure and lamination process differ from liquid coating. It is less common than LPI for many general rigid-board programs.
Screen-applied epoxy mask uses patterned screen printing rather than photoimaging to define the openings. It can suit less dense boards, but it does not offer the same fine-feature freedom as a photoimageable process.
Peelable mask serves a different purpose. It is a temporary protective layer used over selected areas during specific manufacturing operations, then removed. It should not be confused with the permanent insulating coating that remains on the finished PCB.
The practical selection point for an engineer is feature density. A simple board with large through-hole pads can tolerate much larger mask features than a dense ball grid array (BGA) or fine-pitch connector field. As openings move closer together, registration and minimum web width become part of the footprint decision rather than an afterthought in fabrication notes.
How Solder Mask Expansion and Dams Work Together
Solder mask expansion is the offset between the copper pad edge and the mask opening edge. A positive value makes the opening larger than the copper pad. Zero expansion makes the opening nominally the same size. A negative value makes the opening smaller, so the cured coating overlaps the copper edge.
Positive expansion is common because fabrication needs registration margin. If an opening were drawn exactly to the copper edge, an alignment shift could place cured material on part of the solderable pad.
The opening width for a simple rectangular pad can be estimated as:
mask opening = copper pad width + 2 × expansion
That relationship also determines the remaining dam between adjacent openings.
Consider a hypothetical 0.25 mm-wide pad on a 0.50 mm pitch. With 0.05 mm expansion per side, the opening becomes 0.35 mm wide:
0.25 mm + (2 × 0.05 mm) = 0.35 mm
The remaining web between adjacent openings is:
0.50 mm - 0.35 mm = 0.15 mm
Now keep the same 0.25 mm pad but move it to a 0.40 mm pitch. The opening is still 0.35 mm, leaving:
0.40 mm - 0.35 mm = 0.05 mm
If the fabrication target requires at least a 0.08 mm dam, that geometry fails the mask-web rule even though the copper pads themselves still have 0.15 mm of separation.
That is why pad clearance and dam width must be solved together. The engineer has several possible responses:
- Reduce the positive expansion if acceptable registration margin remains.
- Modify pad geometry if the component land pattern permits it.
- Remove the narrow web and use a combined opening where the assembly process can accept it.
- Change the footprint or placement so the mask rule is no longer the limiting feature.
The wrong response is to ignore the violation because the copper design rule check passes. Copper spacing and mask spacing are separate manufacturing constraints.
In the hypothetical baseline above, 0.05 mm expansion per side and a 0.08 mm minimum dam are example values; confirm the actual limits with the fabricator’s DFM review. Dense footprints should still be reviewed feature by feature because a global rule can work on most of the board and fail only inside one package.
Registration Error Is Why Zero Clearance Is Not Automatically Safer
Mask registration is the alignment of the developed opening to the copper feature beneath it. Every fabrication process has some positioning variation, so the design needs enough margin to keep required pad area exposed after imaging and cure.
Increasing expansion gives more protection against mask encroachment on the pad, but it reduces the material left between neighboring openings. Decreasing expansion preserves wider dams, but it reduces the available registration margin. Fine-pitch work is therefore a tolerance trade-off, not a search for the smallest possible number.
Negative expansion is used when the opening is intentionally smaller than the copper pad. That creates a solder-mask-defined pad.
For example, consider a hypothetical circular copper pad with a 0.30 mm diameter and a 0.025 mm contraction on each side. The exposed opening becomes:
0.30 mm - (2 × 0.025 mm) = 0.25 mm
The coating overlaps 0.025 mm of copper around the pad perimeter.
That geometry can be useful where the mask edge is intended to define the exposed solderable area. It also changes the mechanical and assembly conditions at the pad edge, so it should be deliberate. A CAD library that mixes mask-defined and non-mask-defined pads without clear intent can produce inconsistent assembly behavior across the same component field.
For a non-mask-defined pad, the opening extends beyond the copper edge. The copper therefore defines the land geometry while the surrounding coating provides isolation and boundaries around exposed solderable surfaces.
Board A vs Board B: Same Layer Count, Different Mask Risk
Two circuit boards can have the same stackup and thickness yet present very different fabrication risk because of pad pitch and aperture geometry.
| Decision factor | Board A | Board B |
|---|---|---|
| Layer count | 6 layers | 6 layers |
| Board thickness | 1.6 mm | 1.6 mm |
| Example pad width | 0.25 mm | 0.25 mm |
| Example pad pitch | 0.50 mm | 0.40 mm |
| Expansion per side | 0.05 mm | 0.05 mm |
| Calculated opening width | 0.35 mm | 0.35 mm |
| Remaining mask dam | 0.15 mm | 0.05 mm |
| Main DFM issue | Comfortable web between openings | Web falls below a 0.08 mm fabrication target |
Board A leaves enough material between the example openings for the stated target. Board B does not. The layer count, board thickness and copper pad width are identical, but the smaller pitch changes the mask result.
A quotation or manufacturability review based only on layer count misses this difference. Board B may need a footprint adjustment, a smaller opening, or a combined aperture. Each option changes a different part of the tolerance stack.
This is also why fine-pitch layouts should be checked with actual mask openings displayed, not just copper pads. If the CAD view hides top and bottom mask layers during routing, the engineer may not see the remaining web until the final design rule check or fabrication review.
Local exceptions are usually better than changing the global rule. If one package creates a narrow-web violation, reducing expansion for every surface-mount pad can remove useful registration margin from areas that were already manufacturable.
Solder Mask Colors Affect Inspection More Than Electrical Performance
Solder mask colors mainly change visual contrast, appearance and inspection conditions. They do not change the netlist, trace impedance or copper connectivity simply because the pigment is different.
Available options can include green, blue, red, black, white, yellow, purple, matte green and matte black.
Color deserves an engineering check where inspection depends heavily on optical contrast. A dark surface can make some copper and edge details less obvious to a human inspector. A light surface reflects illumination differently. Matte and gloss characteristics can also affect how features appear under inspection lighting.
The legend color should be considered at the same time. A marking system that reads clearly against green material may need another legend color when the board surface changes to white or black.
The engineering question is therefore not which color looks better. It is whether the selected color supports inspection, identification and product requirements without forcing changes to functional geometry.
Do not use pigment choice to solve a spacing problem. A 0.05 mm web does not become acceptable because the coating is green, and a large opening does not become safer because the surface is black. Aperture geometry, registration and cure remain the governing factors.
Treat Vias as a Separate Mask Decision
Vias create a different decision because they may need to stay open, be tented, be plugged, be filled, or be filled and capped depending on electrical, assembly and surface requirements.
Tenting means the mask layer has no opening over the via on the selected side, so cured material covers the via surface. It is a mask decision. Plugging and filling are hole-treatment processes and should not be treated as synonyms for tenting.
A via near a fine-pitch pad can consume valuable mask-web area if it is left open. Tenting that via can remove an unnecessary opening from the mask layer and preserve more material around the component field. The correct treatment still depends on whether the via must remain accessible for test, thermal transfer, plating, filling or another process requirement.
A separate guide on choosing between tented, plugged and filled vias explains those hole treatments as separate fabrication choices rather than interchangeable terms.
Via-in-pad needs further review because the hole sits inside a component land. An open hole can provide a path for molten solder to move away from the pad during assembly. Filled and capped structures address the hole through filling, plating and planarization so the resulting surface can support the component land.
The mask data then has to match the finished pad structure rather than treating the location like an ordinary through via. This is especially relevant in dense BGA escape layouts where vias, pads and aperture boundaries compete for the same small area.
Mask Geometry Must Agree With Surface Finish and Silkscreen
The coating is part of a larger exposed-copper system. Surface finish is applied to copper that remains accessible, so the opening helps define where that finish can exist.
The article on ENIG, HASL and OSP surface finishes compares the pad surfaces and assembly implications of those finishes; the mask decision comes earlier by defining which pad areas are exposed for finishing and soldering.
This interaction matters around fine-pitch pads, edge contacts and test points. A surface-finish callout cannot correct an incorrectly sized opening. If part of a pad is covered, the selected finish cannot reach that covered copper.
The reverse problem also matters. An unnecessarily large opening can expose nearby copper that was intended to remain insulated. Apertures therefore belong in the same engineering review as pad geometry and the specified surface treatment.
Silkscreen is another adjacent layer. Legend ink should not cover exposed solderable surfaces, and reference designators need enough clearance to remain legible after the openings are finalized. The guide to legend sizing, placement and marking errors covers that legend layer separately; its job is identification, while the mask layer controls copper coverage and solder access.
The fabrication package should therefore keep copper, mask, surface finish and legend requirements consistent. Treating them as unrelated drawing layers can create conflicts that appear only during CAM review.
What to Put in the Fabrication Package
A clear release package makes mask intent explicit instead of asking CAM to infer it from the footprint library.
Include:
- Top and bottom mask data in the Gerber RS-274X, ODB++ or IPC-2581 package.
- The intended expansion rule where it differs from the normal board rule.
- Any intentionally mask-defined pads.
- Via treatment instructions for open, tented, plugged, filled or capped structures.
- Areas where combined openings are intentional.
- Color and finish requirements.
- Peelable protection requirements, if used.
- Fabrication notes identifying any local exception to the general rule.
Also run a dedicated design rule check for minimum mask sliver or web width. A copper-spacing rule will not catch every aperture problem because the copper edge and mask-opening edge are different geometries.
The released data also needs to agree across files. A fabrication note that specifies one treatment while the mask Gerber shows another leaves the manufacturer with conflicting instructions. Resolve those conflicts before release rather than relying on CAM interpretation.
Likewise, avoid a generic instruction such as “adjust mask as required” where a particular aperture is functionally significant. If exposed copper area matters to the component, connector, test point or spacing strategy, define the requirement clearly enough for engineering review.
Send Your Fabrication Files
Send your Gerbers or ODB++, drill files and fabrication drawing. Every board gets an engineer-reviewed DFM check before fabrication starts, under an ISO 9001:2015 certified quality system. Request a quote or send your files to sales@rlxsolutions.com.
Frequently Asked Questions
What is the difference between solder mask and paste mask?
Solder mask is the permanent cured coating that covers copper and defines exposed pad areas on the finished PCB. Paste mask is assembly data used to define stencil apertures for solder paste deposition. The two layers interact around component lands, but they control different processes and should not be treated as interchangeable fabrication files.
Can solder mask cover vias?
Yes. A via can be tented by closing the mask opening on one or both sides, which leaves cured coating over the via surface. That is different from plugging or filling the hole. Whether a via should stay open or be covered depends on test access, assembly geometry and the required via treatment.
What happens if the mask overlaps a component pad?
Unintended overlap reduces the exposed solderable area and can change wetting around the pad. On fine-pitch parts, even small encroachment can create unequal pad exposure across the footprint. Positive opening clearance is commonly used to provide registration margin, while intentionally mask-defined pads use controlled overlap as part of the land design.
Is black mask harder to inspect than green?
It can be more demanding for visual inspection because dark surfaces provide different contrast against traces, pads and markings. Inspection systems can be configured for different colors, so black is not automatically unacceptable. The engineering question is whether the chosen color supports the required optical inspection and legend contrast without changing board geometry.
What files should I send for a PCB with special mask requirements?
Send the manufacturing data that defines copper, mask, drill and board outline, such as Gerber RS-274X, ODB++ or IPC-2581, plus NC drill data and relevant fabrication notes. If special openings, via treatment or mask-defined pads are intentional, identify those exceptions clearly so they can be reviewed against the actual board geometry.
Pingback: Silkscreen PCB Rules, Fonts & Mistakes | RLX Solutions